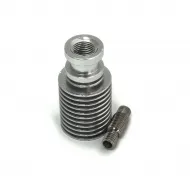


- Stock: Out of Stock
- Model: Nozzle-1.75 hardened steel-0.6

Model:

Clon V6 0.1
Clon V6 0.25
Clon V6 0.3

Clon V6 0.35

Clon V6 0.4

Clon V6 0.5

Clon V6 0.6

Clon V6 0.8

TV6 0.3

TV6 0.4

TV6 0.5

Hardened Steel 0.4

Hardened Steel 0.5
Hardened Steel 0.6

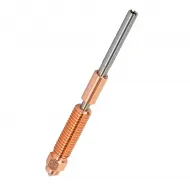
Plated Copper 0.4

Plated Copper 0.6

Plated copper and 0.4 hardened steel tip

Plated copper and 0.6 hardened steel tip
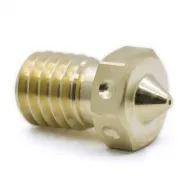
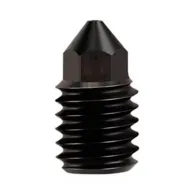
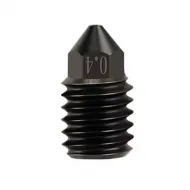
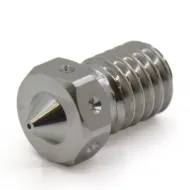
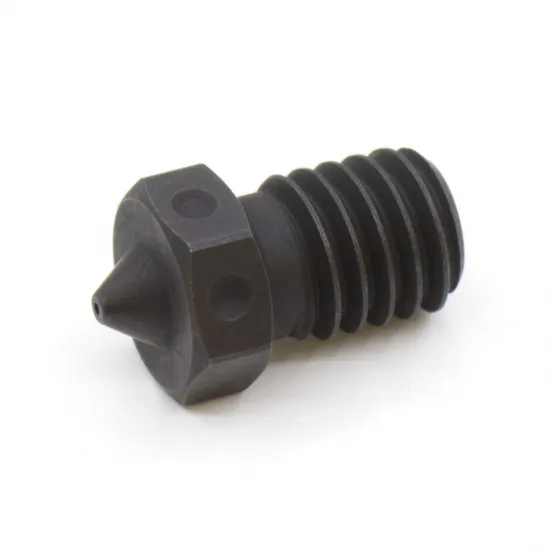
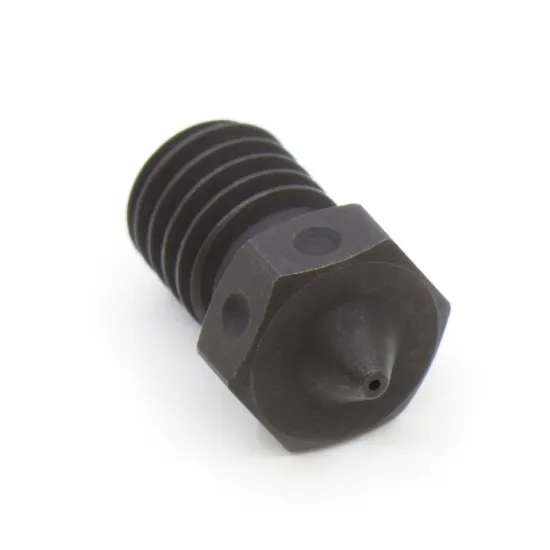
A 0.6 mm Trianglelab V6 nozzle made from hardened A2 tool steel with a declared hardness of HRC 62. Its combination of wear resistance and a larger outlet is particularly useful for 1.75 mm carbon-fibre, glow-in-the-dark, wood-filled, metal-filled and other abrasive filaments.
Compared with 0.4 and 0.5 mm, the 0.6 mm outlet provides more relative clearance for filled materials and supports wider lines and layers. It cannot prevent every clog, so the filament manufacturer's minimum diameter must still be observed. It also does not guarantee faster printing by itself because melt flow remains limited by the hotend.
Technical specifications
| Feature | Value |
|---|---|
| Brand and family | Trianglelab A2 Hardened Steel V6 |
| Material | Hardened A2 steel |
| Declared hardness | HRC 62 |
| Outlet diameter | 0.6 mm |
| Filament | 1.75 mm |
| Nominal thread | M6 × 1 |
| Nominal V6 length | 12.5 mm |
| Spanner size | 7 mm |
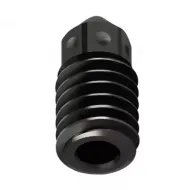
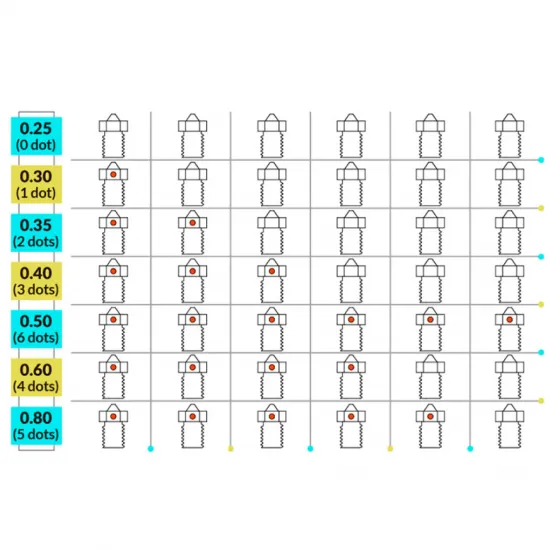
| Identification | 4 dots on the hex |
| Contents | 1 nozzle |
Its dark finish may show minor colour or texture variation as a result of thermal and chemical treatment. Trianglelab describes these variations as normal and non-functional.
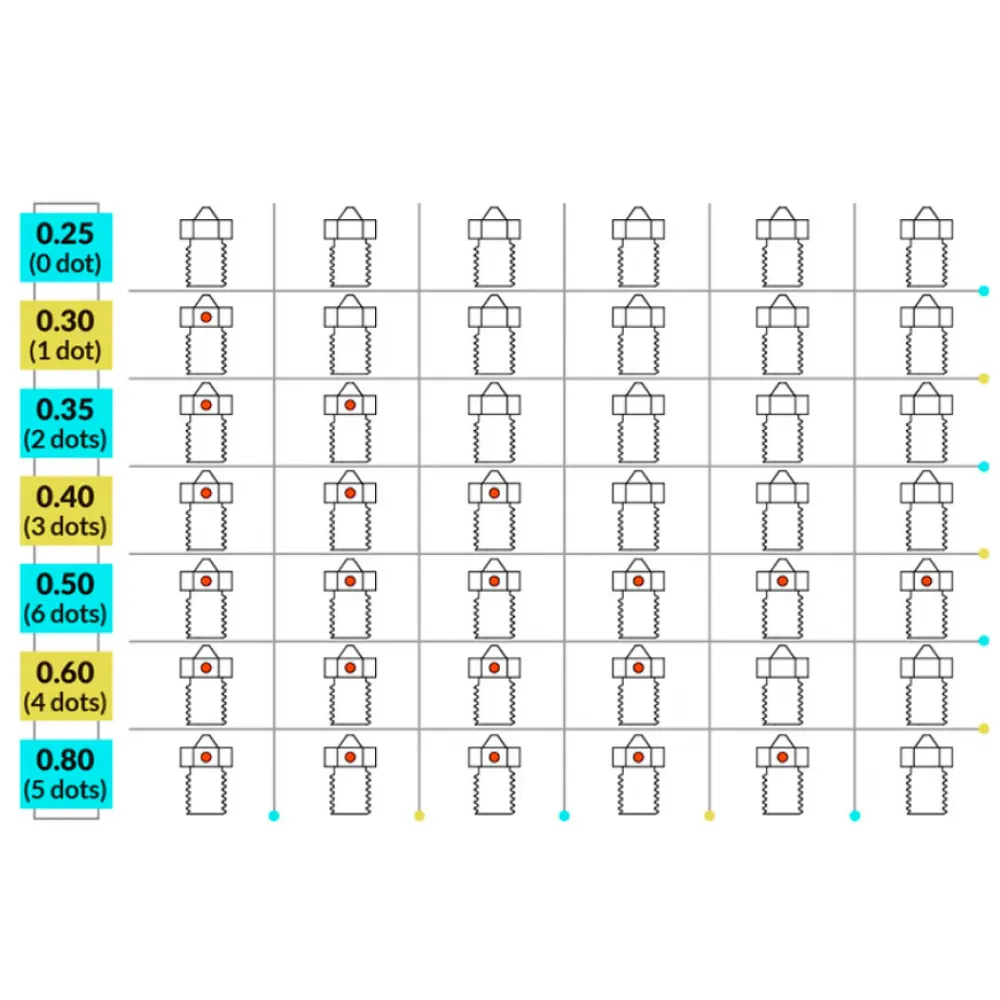
Diameter comparison
| Diameter | Dots | Typical choice |
|---|---|---|
| 0.4 mm | 3 | More detail; check filler particle size particularly carefully. |
| 0.5 mm | 6 | Balance between detail, line width and particle clearance. |
| 0.6 mm — this product | 4 | Wider lines and layers with lower relative sensitivity to filled materials. |
Compatibility
Compatible with V6 hotsides for 1.75 mm filament that share the same M6 × 1 thread, length and sealing geometry. Trianglelab declares compatibility with V6, Lite6 and Titan Aero. On Prusa and other printers, direct compatibility should only be claimed when the installed hotend retains this V6 interface.
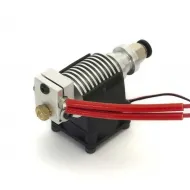
It may be used with the V6 All Metal hotend for 1.75 mm filament or a Trianglelab Brass V6 heater block for 3 mm sensors, while also checking the heatbreak, thread engagement and clearance around the nozzle tip.
Installation and tightening
- Unload filament and use tools and protection suitable for a hot assembly.
- Start the thread gently. The seal must form between the nozzle and heatbreak inside the block.
- Support the block and hot-tighten. As a V6 hardened-steel reference, E3D specifies approximately 20 °C above the intended print temperature, about one minute of stabilisation and 2 N·m with a 7 mm spanner. Specific hotend instructions take precedence if they differ.
- Maintain a small visible gap between the hex and block and inspect for leakage after heating and cooling.
The 6 and 7 mm open-ended spanner operates the nozzle hex, while the multi-purpose heater-block tool helps prevent torque from reaching the heatbreak. Excess torque can shear components.
0.6 mm profile and firmware
- Select 0.6 mm in the slicer, slice again and review line widths, layer heights, speed and volumetric flow.
- A wider line consumes more material per second. If the hotend cannot melt it, reduce speed or line width even though the outlet is larger.
- Steel's lower thermal conductivity than Brass may call for a slightly higher temperature or lower speed. Determine this by calibration without exceeding safe limits.
- In Marlin and RepRapFirmware, the change is normally handled by the slicer and does not require universal firmware recompilation.
- In Klipper, set
nozzle_diameter: 0.6under[extruder], runRESTARTand use newly sliced G-code.
Temperature and cleaning
The safe temperature is set by the lowest-rated component in the complete hotside. Trianglelab's mention of PEEK or PEI does not prove that the sensor, block, heater, heatbreak, wiring, firmware or printer is suitable for them.
For clearing or changing material, prefer cleaning filament and warm or cold pulls. Carefully clean the exterior with a Brass brush. Avoid blowtorches, steel brushes, needles that may alter the outlet and disassembly while cold.