- Stock: 1
- Model: ABS-RE-WINKLE

Range

ABS

ABS RE
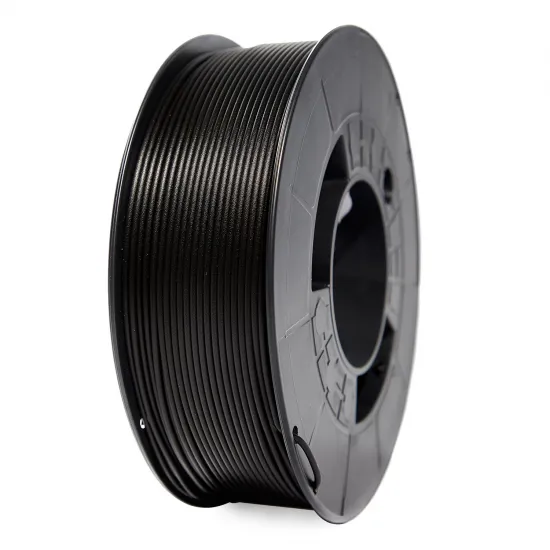
WINKLE recycled ABS RE filament in 1.75 mm is made in Spain from surplus material generated during the production of other filaments within a similar colour range. It offers a practical way to reuse manufacturing material for functional ABS prints when an exact shade is not essential to the project.
Key features
- Material: ABS RE made from production surplus.
- Manufactured in: Spain.
- Nominal diameter: 1.75 mm.
- Contents: 1 kg spool.
- Colour: recycled and variable; not selectable.
- Technology: FFF/FDM 3D printers prepared for ABS.
- Packaging: sealed bag to help protect the material from moisture and light.
Printing settings: starting point
The ABS RE reference is no longer listed in WINKLE's current range, so it should not be assumed to share every property of today's standard ABS. The values below use current WINKLE ABS documentation as a reference and should be adjusted with a short test for the particular spool, printer and geometry.
| Setting | Suggested starting value |
|---|---|
| Nozzle temperature | 230–260 °C |
| Bed temperature | 80–100 °C |
| Print speed | 50–70 mm/s; reduce it for large parts or if layer bonding is insufficient |
| Enclosure | Enclosed or protected from draughts, particularly for large parts |
| Nozzle | 0.4 mm as a common reference; other diameters require flow, layer height and speed recalibration |
Start near the middle of each range and assess finish, layer bonding and corner stability. If the edges lift, first check cleanliness, levelling, first-layer setup, bed temperature and draughts. For demanding geometries, a heated-bed adhesive such as DIMAFIX Pen may help, provided that its instructions and those of the build surface are followed.
3D printer compatibility
At material level, it is suitable for 1.75 mm FFF/FDM printers that can reach the required temperatures and use a suitable build surface. An HPRO prepared for ABS, an enclosed Voron or enclosed machines such as the Bambu Lab P1S, X1, X1 Carbon and X1E are reasonable candidates, but every combination still needs its own profile and a supervised first test.
WINKLE currently publishes standard ABS profiles for the Bambu Lab P1S, P1P, X1, X1 Carbon and X1E. They may provide a starting reference, but they are not profiles validated specifically for this ABS RE. Open printers such as the Creality Ender-3, Prusa MK3/MK4, Bambu Lab A1/A1 mini and similar designs face a greater risk of warping and layer separation, especially on large parts.
Compatibility with AMS, AMS Lite, MMU or other automatic material systems cannot be guaranteed from diameter alone. Check that the spool fits and rotates freely, and that the filament in the supplied batch is not too curved or brittle for the complete feed path.
Safe printing and storage
- Print in a well-ventilated space and avoid remaining next to the machine while breathing the fumes.
- An enclosure helps to stabilise temperature, but it must not trap power supplies or electronics that are not designed for a warmer ambient environment.
- Store the spool sealed, dry and away from direct sunlight, preferably with silica gel.
- If bubbles, popping sounds or a rough surface appear, check for moisture before making major profile changes. Use only a drying process suitable for ABS and for the spool itself.
- Print a test part before a long production run: recycled origin and potential batch variation make it advisable to validate temperature, flow and finish.
It is for you if
- You need 1.75 mm ABS for functional parts and the exact colour is not critical.
- You want to use a reference made from production surplus.
- Your printer has a heated bed, suitable temperatures and protection from draughts.
- You can run a short calibration test for each spool or batch.
It is not for you if
- You need to reproduce exactly the same shade across parts or later orders.
- You require a tightly specified profile with certified mechanical properties for calculation or critical use.
- Your machine cannot maintain the necessary temperatures or is exposed to draughts.
- The part will remain outdoors under prolonged sunlight: in that case, consider WINKLE ASA filament instead.
If you prefer defined colours and a currently documented WINKLE formulation, see the standard WINKLE ABS 1.75 mm filament.