

- Stock: Out of Stock
- Model: Inserto-M5
Type:

M3

M4

M5
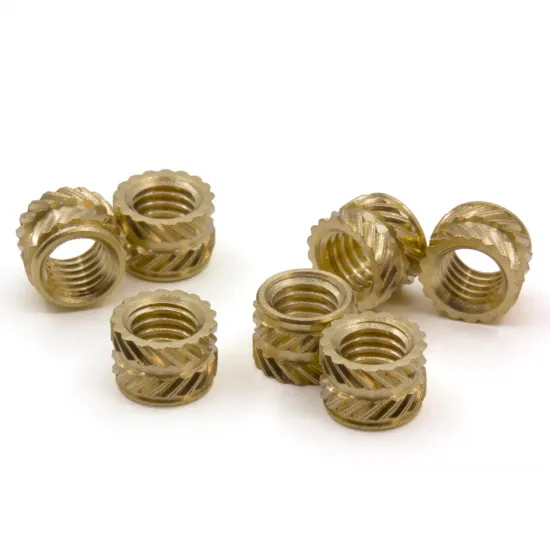
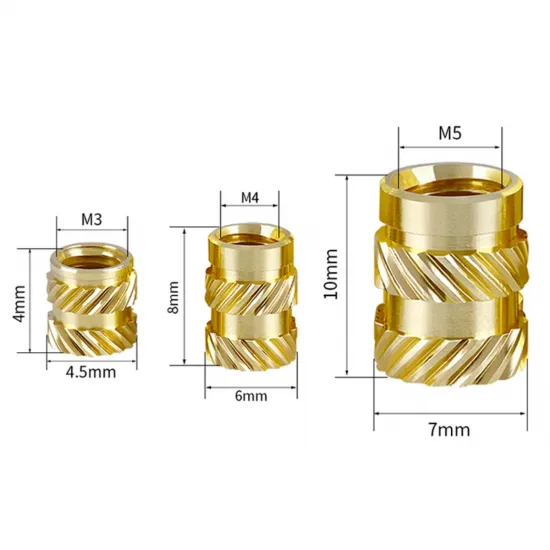
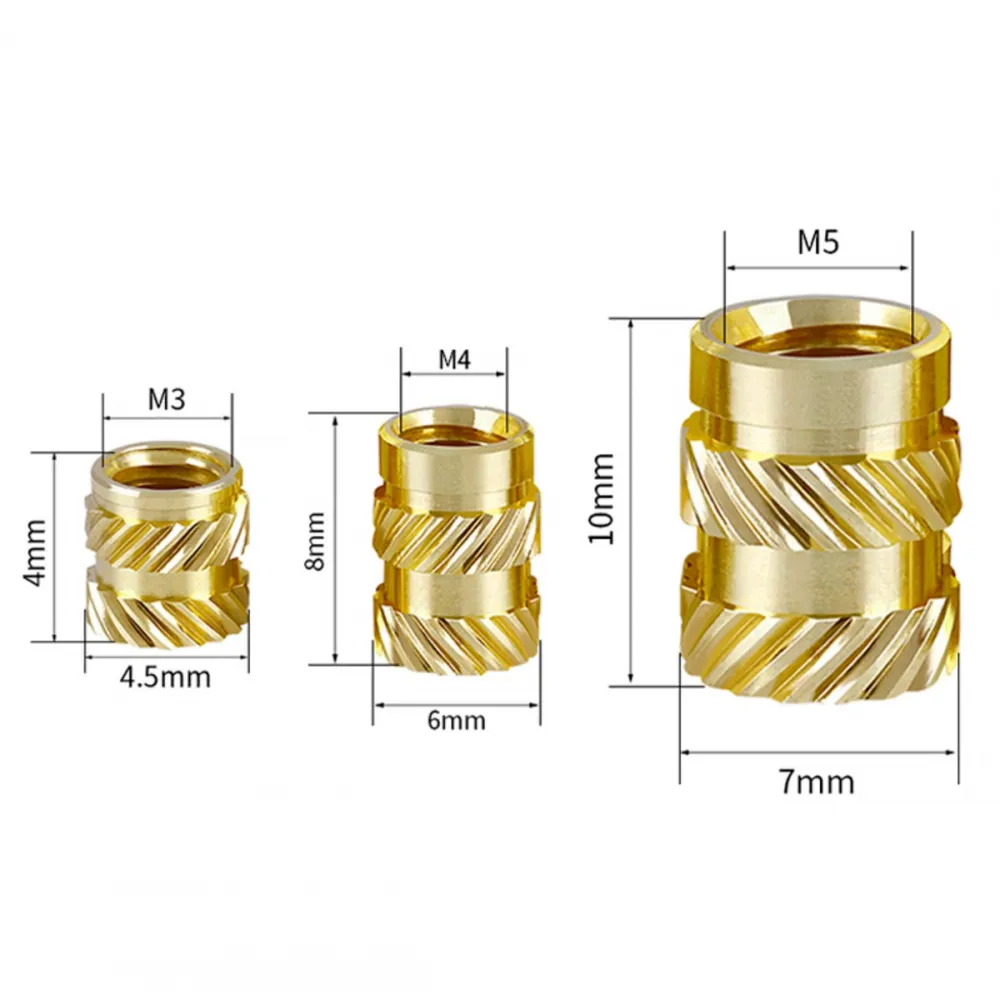
M5 Brass threaded insert for adding a durable, reusable metal thread to thermoplastic parts. Its Ø7 × 10mm body and bidirectional external knurling provide a large contact area with the surrounding material.
It is intended for larger printed components, mechanical brackets, enclosures and parts using M5 hardware. Its dimensions require more space and supporting material than the M3 and M4 versions.
Features and dimensions
- Internal thread: M5.
- Nominal outside diameter: 7mm.
- Nominal length: 10mm.
- Material: Brass, a copper alloy.
- Thread: through-threaded.
- External surface: opposing diagonal knurls.
- Primarily designed for thermal insertion into thermoplastics.
Sales unit
The price is for one insert. The screw and heat-setting tool are not included.
Typical applications
- Medium-sized printed structural brackets.
- Mounting motors and mechanical components.
- Enclosures requiring repeated opening and closing.
- Fixtures, robots and custom machinery.
- Removable joints using M5 hardware.
Part requirements
The receiving hole must accommodate an insert measuring 7mm in outside diameter and 10mm long. Sufficient surrounding material is required to withstand both installation and subsequent loads.
- Do not position it next to an excessively thin outside wall.
- Allow additional depth for displaced plastic.
- Make sure the screw cannot bottom out.
- Add perimeters or local reinforcement when the joint will carry loads.
- Print a test piece before manufacturing a large or expensive component.
Thermal installation
- Centre the insert over the receiving hole.
- Heat it using a temperature-controlled tool and suitable tip.
- Press it in slowly and perpendicular to the surface.
- Stop applying pressure when it becomes flush.
- Hold it still until the thermoplastic solidifies.
- Check alignment before installing the M5 screw.
If the insert remains slightly raised, it may be corrected with a second brief application of heat. Do not hammer or force it in cold, as this may crack the part or separate its printed layers.
Selecting the screw
The screw must match both the nominal diameter and thread pitch. Its length must provide sufficient engagement without entering an unintended area, bottoming out or pushing the insert from the part.
Thread pitch, tolerance, maximum torque and pull-out strength are not specified. Test the complete joint when it will carry significant loads.
Compatible materials
Primarily intended for PLA, PETG, ABS, ASA, PA and other thermoplastics that can soften around the knurling. Installation temperature and receiving-hole diameter must be adjusted for each material.
It should not be installed using the same heat-setting process in thermoset resin, wood, metal or other materials that do not melt in a controlled manner.