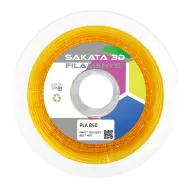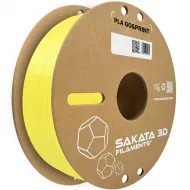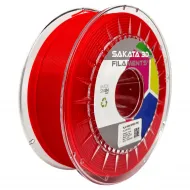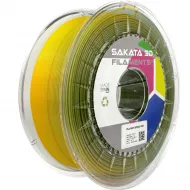
- Stock: 12
- Model: PLA-Go&Print-Transition

Type:

PLA GO&PRINT

GO&PRINT Transition

GO&PRINT Recycled

PLA-M

PLA-M Transition

PLA 3D850

PLA INGEO 3D850 Fluor

PLA 3D850 MAGIC / MAGIC+

PLA 3D850 SILK

PLA 3D850 GLASS

PLA 3D850 Transition

3D850 Recycled

HR-PLA 3D870

HR-PLA 3D870 Transition

Recycled 3D870

PLA High Speed

PLA High Speed PRO

PLA High Speed PRO TransitionHigh Speed
Sakata 3D PLA GO&PRINT Transition consists of spools produced while changing between two colours in the GO&PRINT range. It retains the technical specifications of the material, but its colour combination falls outside the standard commercial colour chart.
It may contain two shades, an intermediate mixture or such a subtle change that it is barely noticeable. The colour combination, intensity, position and length of the transition are random.
Product images are illustrative only. The supplied spool is not guaranteed to contain the colours shown, a clearly visible transition, a particular gradient or a rainbow effect.
Particularly suitable for
- Prototypes and early design iterations.
- Dimensional and functional tests.
- Tools, supports and internal or hidden components.
- Large parts where an exact colour is not essential.
- Decorative projects that can make use of a unique and unpredictable colour combination.
Main features
- Manufactured in Spain by Sakata 3D.
- PLA GO&PRINT produced during manufacturing colour changes.
- Nominal diameter of 1.75mm with a ±0.03mm tolerance.
- 1kg spool.
- Uses the same general printing recommendations as standard GO&PRINT.
- Colour, transition and colour distribution cannot be selected.
- No heated enclosure required.
Technical parameters
| Material | PLA GO&PRINT Transition |
|---|---|
| Diameter | 1.75 ±0.03mm |
| Net weight | 1kg |
| Density | 1.24g/cm³ |
| Nozzle temperature | 185–200°C for conventional printing; 200–240°C for high-speed printing |
| Heated bed | From 45°C; 50–55°C is a practical starting point |
| Part cooling | Up to 100% after the first layers |
| Suggested layer height | 0.10–0.30mm |
| Colour | Random; transition may be visible, subtle or unnoticeable |
Suggested starting profile
Start with a 195°C nozzle, 50–55°C bed, 50–70mm/s print speed and 100% part cooling after the first layers. These values should be adjusted for the hotend, build surface and part geometry.
Although the material supports fast printing, speed should be increased gradually and kept within the hotend’s actual melting capacity to prevent under-extrusion or reduced interlayer bonding.
Compatibility
Suitable for FFF/FDM printers designed for 1.75mm filament, including common Creality Ender 3, Prusa MK3/MK4, Bambu Lab A1/P1/X1, Voron and HTA3D configurations. Check the feed system, spool holder and printing profile before use.
For automatic material systems, spool compatibility should be verified beforehand. When compatibility with the particular feeder is not confirmed, using an external spool holder is recommended.
Storage
Keep protected from moisture and store sealed, preferably with desiccant. If popping, bubbles or an uneven surface appear, it can be dried for approximately 4–6 hours at 55°C.
The product is not specifically certified for food-contact or medical applications. Its colour does not remove the need to validate the mechanical properties of each printed part.
For a selectable commercial shade, choose standard Sakata 3D PLA GO&PRINT. To make use of material recovered from the production process, consider Sakata 3D RE-GO&PRINT recycled filament.