- Stock: 18
- Model: PLA-Go&Print 1.75mm-SAKATA3D

Type:

PLA GO&PRINT

GO&PRINT Transition

GO&PRINT Recycled

PLA-M

PLA-M Transition

PLA 3D850

PLA INGEO 3D850 Fluor

PLA 3D850 MAGIC / MAGIC+

PLA 3D850 SILK

PLA 3D850 GLASS

PLA 3D850 Transition

3D850 Recycled

HR-PLA 3D870

HR-PLA 3D870 Transition

Recycled 3D870

PLA High Speed

PLA High Speed PRO

PLA High Speed PRO TransitionHigh Speed
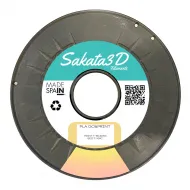
Sakata 3D RE-GO&PRINT is a PLA filament manufactured in Spain from GO&PRINT material recovered from Sakata 3D’s own production process. It makes use of material that would otherwise become waste while retaining printing characteristics similar to the GO&PRINT family.
The recovered material comes from the manufacturer’s own GO&PRINT production, with no externally sourced recycled PLA resin added. It is particularly suitable for prototypes, tools, functional parts and tests where exact colour consistency is not essential.
Variable colour
The shade depends on the mixture of colours recovered during production. Therefore, colour can vary between batches, between spools and even along the same spool. Product images are illustrative, and a particular colour or completely uniform shade cannot be guaranteed.
Main features
- Manufactured in Spain by Sakata 3D.
- Made entirely from GO&PRINT material recovered from the manufacturer’s production process.
- Nominal diameter of 1.75mm with a ±0.05mm tolerance.
- 1kg spool.
- Low warping and straightforward printing.
- No heated enclosure required.
- Variable, non-selectable colour.
Technical parameters
| Material | Recovered PLA RE-GO&PRINT |
|---|---|
| Diameter | 1.75 ±0.05mm |
| Net weight | 1kg |
| Density | 1.24g/cm³ |
| Nozzle temperature | 185–205°C |
| Heated bed | Not essential; optional 50–70°C depending on the surface and part |
| Part cooling | Up to 100% after the first layers |
| Suggested layer height | 0.10–0.30mm |
| Stated maximum speed | Up to 120mm/s, subject to printer capability and part geometry |
| Colour | Variable, random and without a uniformity guarantee |
Suggested starting profile
A practical starting point is a 195°C nozzle, 50°C bed when required by the surface, 50–70mm/s print speed and 100% part cooling after the first layers. Temperature, flow and retraction should be adjusted with a short test before printing large parts.
Compatibility
Suitable for FFF/FDM printers using 1.75mm filament, including common Creality Ender 3, Prusa MK3/MK4, Bambu Lab A1/P1/X1, Voron and HTA3D configurations. Final compatibility depends on the feed system, hotend, spool holder and print profile.
For automatic material systems, check spool compatibility and confirm that the filament moves freely. If excessive resistance is detected or the particular feeder is not confirmed, use an external spool holder.
Storage
Store in a sealed bag or container, preferably with desiccant. If the filament produces bubbles, popping sounds or an uneven surface, dry it using a suitable PLA drying procedure.
It is not specifically certified for food-contact or medical applications. The properties of a printed part also depend on orientation, infill, perimeter count, temperature and interlayer bonding.
When a selectable commercial colour and tighter dimensional tolerance are required, choose standard Sakata 3D PLA GO&PRINT. GO&PRINT Transition is another option for applications where unpredictable colour changes are acceptable.