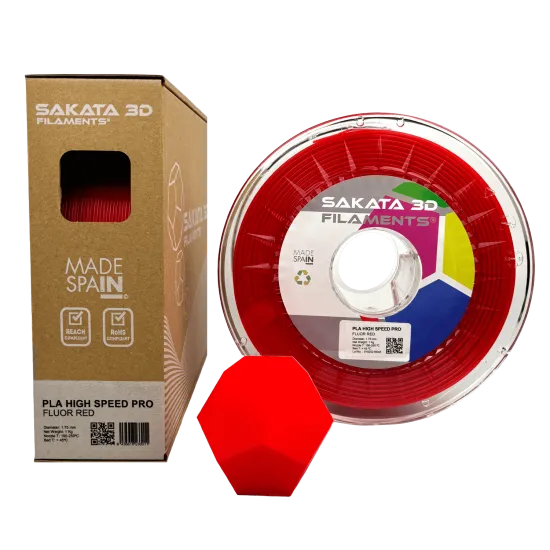
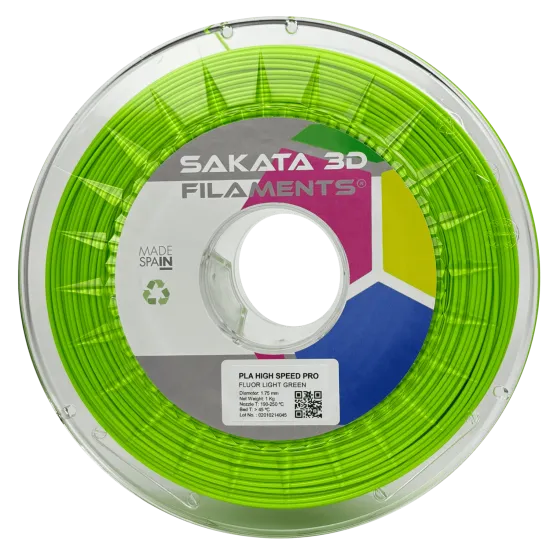
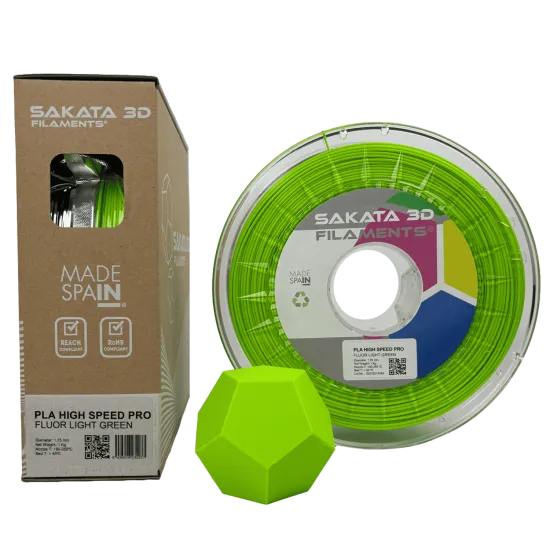
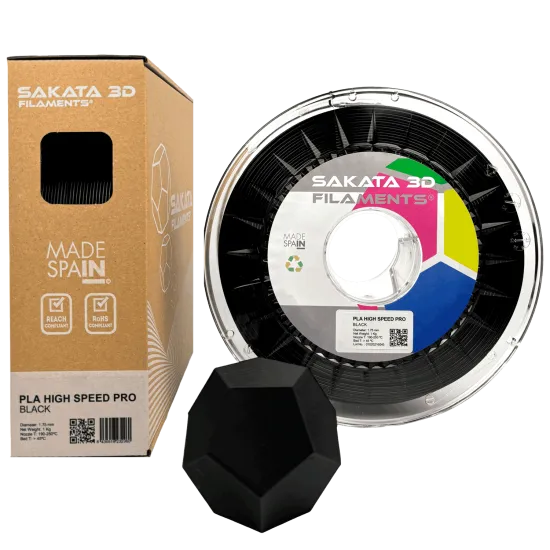


- Stock: 38
- Model: PLA-HS-PRO-1.75mm-SAKATA3D

Type:

PLA GO&PRINT

GO&PRINT Transition

GO&PRINT Recycled

PLA-M

PLA-M Transition

PLA 3D850

PLA INGEO 3D850 Fluor

PLA 3D850 MAGIC / MAGIC+

PLA 3D850 SILK

PLA 3D850 GLASS

PLA 3D850 Transition

3D850 Recycled

HR-PLA 3D870

HR-PLA 3D870 Transition

Recycled 3D870

PLA High Speed

PLA High Speed PRO

PLA High Speed PRO TransitionHigh Speed
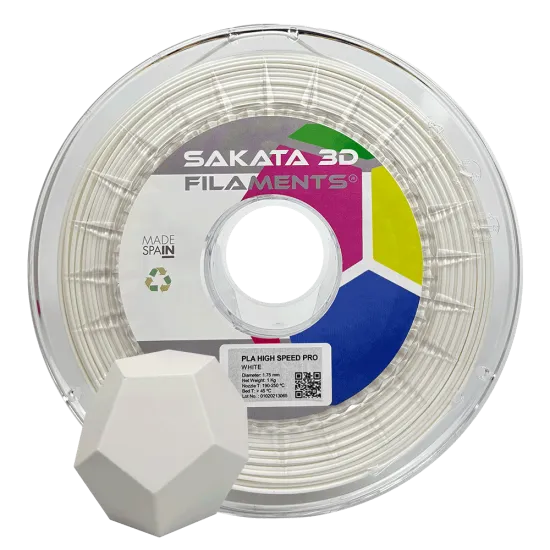
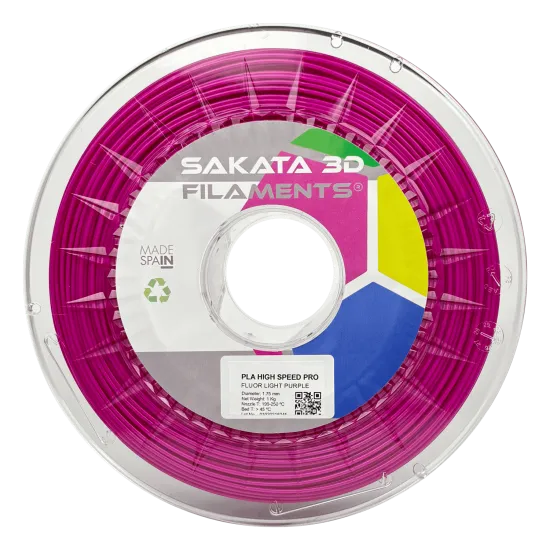
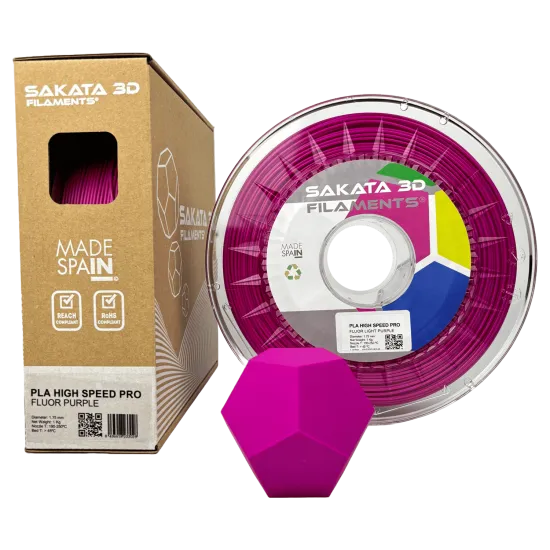
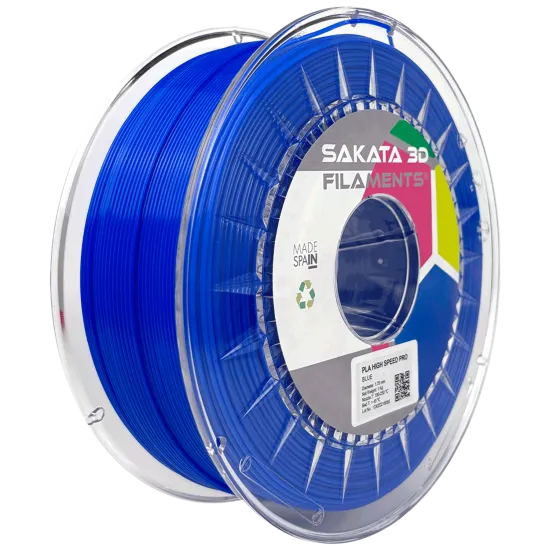
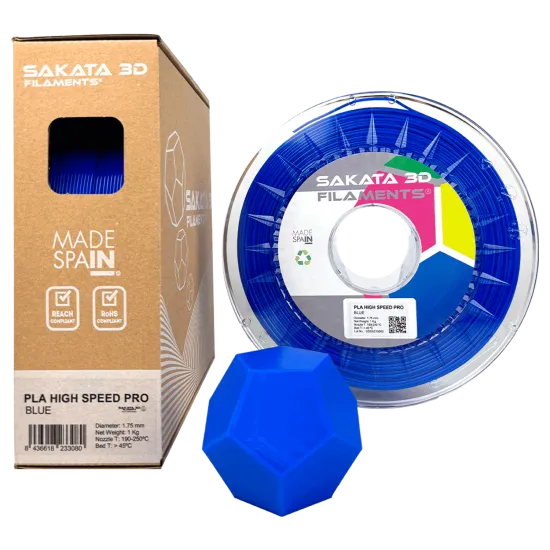
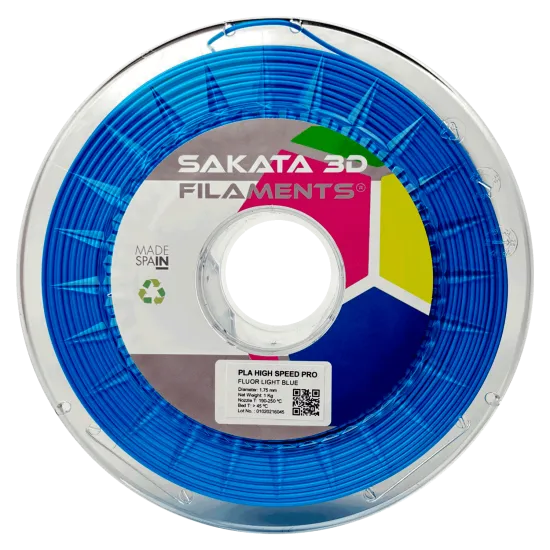
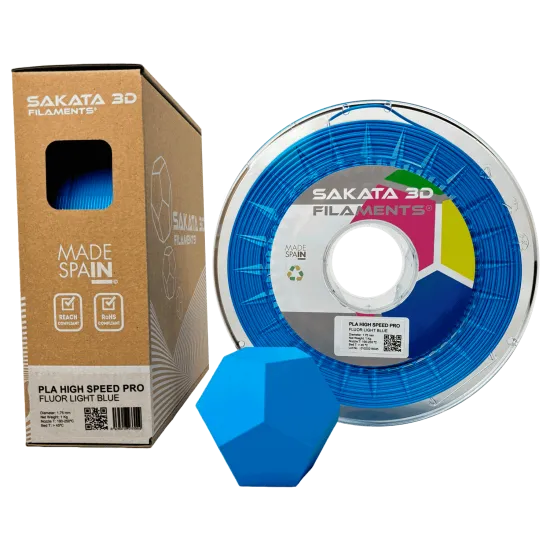
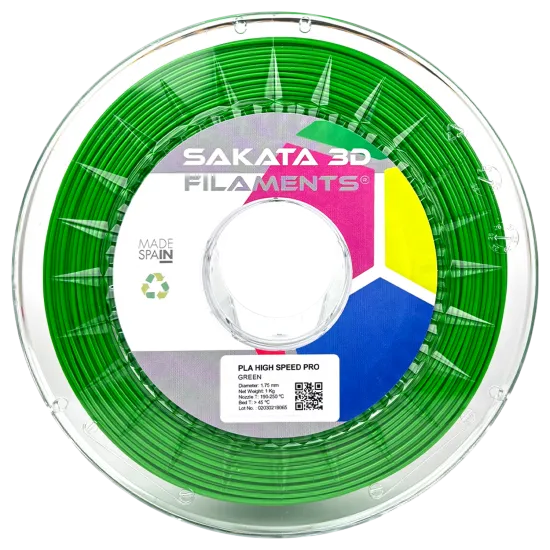
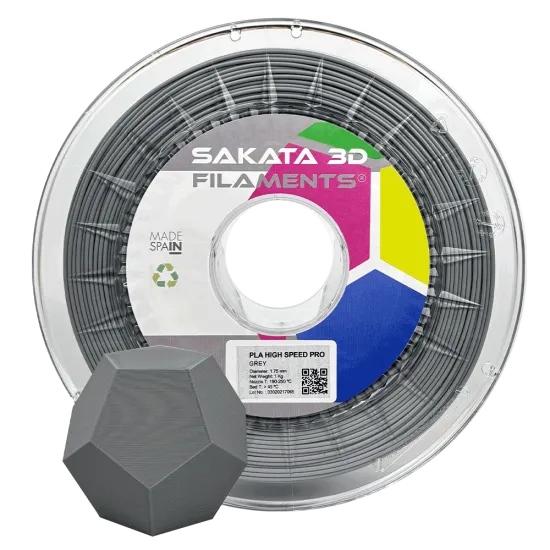
Sakata 3D PLA High Speed PRO is a 1.75 mm PLA filament made in Spain and developed for both conventional and high-speed printing profiles. Its technical data sheet covers 50–100 mm/s in a classic profile and 100–500 mm/s in fast machines, with a declared maximum volumetric flow of 24 mm³/s under the manufacturer's test conditions.
Final speed depends on more than the filament: hotend, nozzle, extruder, acceleration, layer height, line width and geometry may impose a lower limit. It can therefore also be used as conventional PLA, starting with a conservative profile and increasing temperature and flow gradually.
Main features
- Brand: Sakata 3D, made in Spain.
- Material: PLA High Speed PRO.
- Diameter: 1.75 ±0.03 mm.
- Roundness: maximum deviation of 0.03 mm.
- Net weight: 1 kg.
- Classic speed: 50–100 mm/s.
- High-speed range: 100–500 mm/s, subject to a declared maximum flow of 24 mm³/s.
- Nozzle: Sakata 3D bases its settings on a 0.4 mm Brass nozzle.
- Bed: above 45 °C on glass or PEI.
- Enclosure: not required.
- Part cooling: 100% in the official reference profile.
Recommended print settings
| Setting | Classic profile | High-speed profile |
|---|---|---|
| Nozzle temperature | 190–210 °C | 210–250 °C |
| Linear speed | 50–100 mm/s | 100–500 mm/s |
| Volumetric flow | Match the hotend | Up to 24 mm³/s declared |
| Bed temperature | Above 45 °C | |
| Surface | Glass or PEI; adhesive spray or stick when needed | |
| Cooling fan | 100% | |
| Layer height | 0.1–0.3 mm | |
| Enclosure | Not required | |
| Optional drying | 6–8 h at 45 °C; dry box at 45 °C during printing if required | |
These values are Sakata 3D starting points based on a 0.4 mm nozzle. Set temperature and maximum flow first, then tune retraction, flow ratio, pressure advance or linear advance and speed for the actual machine.
500 mm/s does not mean 500 mm/s on every layer
The slicer converts speed, line width and layer height into flow. At the declared 24 mm³/s maximum and a 0.45 mm line, the theoretical limit changes as follows:
| Layer height | Line width | Theoretical speed at 24 mm³/s |
|---|---|---|
| 0.10 mm | 0.45 mm | 533 mm/s; also capped at 500 mm/s by the TDS |
| 0.20 mm | 0.45 mm | 267 mm/s |
| 0.30 mm | 0.45 mm | 178 mm/s |
These are geometric calculations, not guaranteed speeds. Small walls, overhangs, bridges, first layers and parts with constant direction changes usually run slower. The hotend may also reach less than 24 mm³/s with a different temperature, nozzle or environment.
Reference properties
| Property | Standard | Value |
|---|---|---|
| Density | ASTM D1505 | 1.24 g/cm³ |
| Tensile modulus | ASTM D638 | 3,365 MPa |
| Tensile strength | ASTM D638 | 64 MPa |
| Flexural modulus | ASTM D790 | 3,633 MPa |
| Flexural strength | ASTM D790 | 112 MPa |
| HDT at 0.45 MPa | ASTM E2092 | 55 °C |
3D printer compatibility
Its 1.75 mm format suits FFF/FDM printers able to process PLA. It can be configured for HTA3D HPRO 330/400, Bambu Lab A1, A1 mini, P1P, P1S and X1; Creality K1, K1C, K1 Max and Ender-3 V3; Prusa MK4/MK4S, XL and Core One; and Voron V0.2, Trident or 2.4, provided that hotend, extruder, nozzle, cooling and profile are suitable.
On a basic printer it can run at conventional speed. On a fast machine, start from the printer manufacturer's profile and increase flow only after checking extrusion, layer bonding and finish. Do not convert the machine's travel-speed limit directly into print speed.
HTA3D declares an approximately 195 mm diameter, 70 mm wide spool with a 53 mm centre bore. Check clearance in AMS, MMU, dryers and enclosed spool holders; an external holder may be required.
It is for you if
- You want a European PLA for both conventional and fast printing.
- Your machine lets you calibrate maximum flow and temperature for speed.
- You want strong part cooling and low warping without requiring an enclosure.
- You need a 1 kg spool with controlled 1.75 ±0.03 mm diameter.
It is not for you if
- You need a part for continuous service clearly above the PLA reference HDT.
- You require food-contact or medical certification.
- You expect every geometry to print at 500 mm/s without flow, temperature and acceleration tuning.
- Your enclosed feeder cannot accept an approximately 195 × 70 mm spool.
Storage and drying
Keep the spool sealed and protected from moisture, dust and heat. If popping, bubbles, unusual stringing or a rough surface appear, Sakata 3D gives an optional drying setting of 6–8 hours at 45 °C. The filament can also be fed from a dry box at 45 °C during printing. Use accurately controlled equipment and avoid deforming the spool.
Provide good general ventilation. Although the manufacturer describes the material as biodegradable, this should not be interpreted as home-compostable or as permission to discard prints in the environment.
Other options
For unpredictable colour changes with the same formulation, see Sakata 3D PLA High Speed PRO Transition. If a matte finish and reduced layer visibility matter more than maximum flow, consider Sakata 3D PLA-M.
Package contents
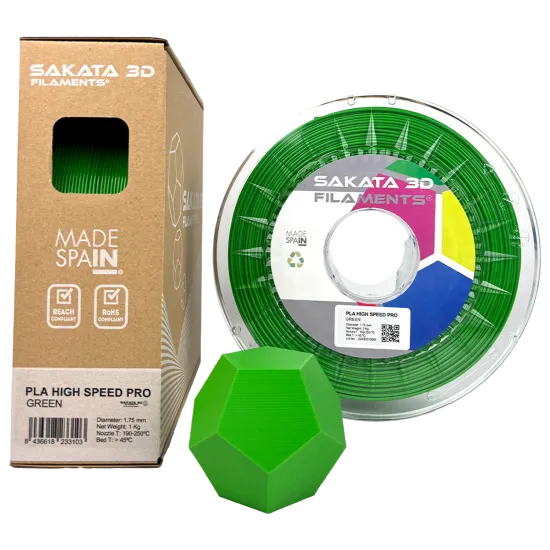
- 1 spool of Sakata 3D PLA High Speed PRO.
- Diameter: 1.75 mm.
- Net weight: 1 kg.
- Vacuum packed with desiccant.
Technical documentation
Settings and properties are taken from the official Sakata 3D PLA HS PRO technical data sheet, revision 10 April 2025.