

- Stock: 4
- Model: ADXL345 V2.0

Type:

S2DW

ADXL345
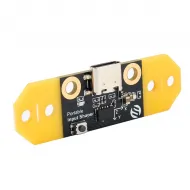
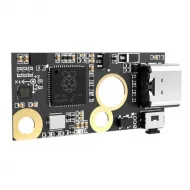
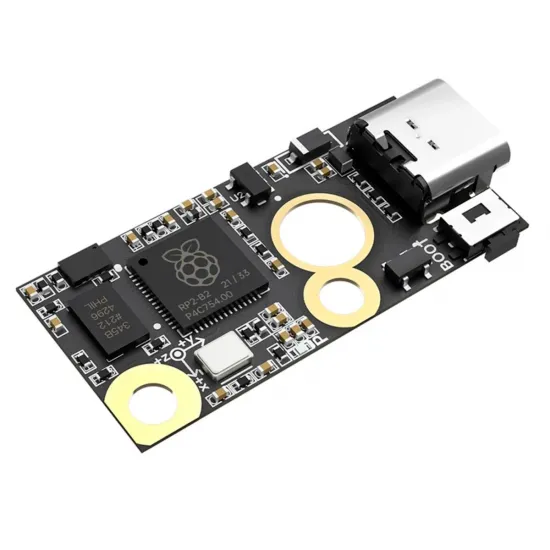
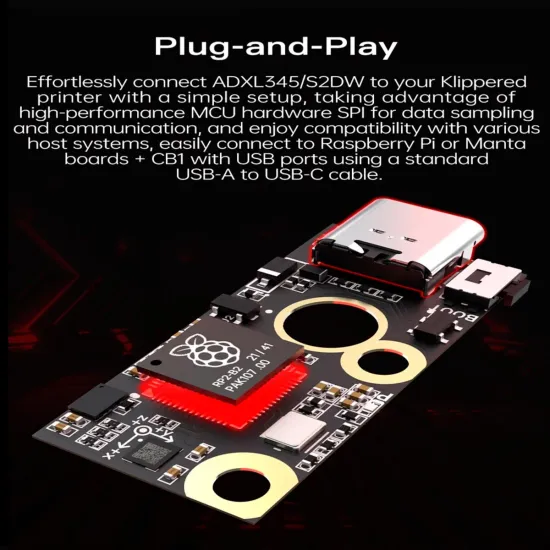
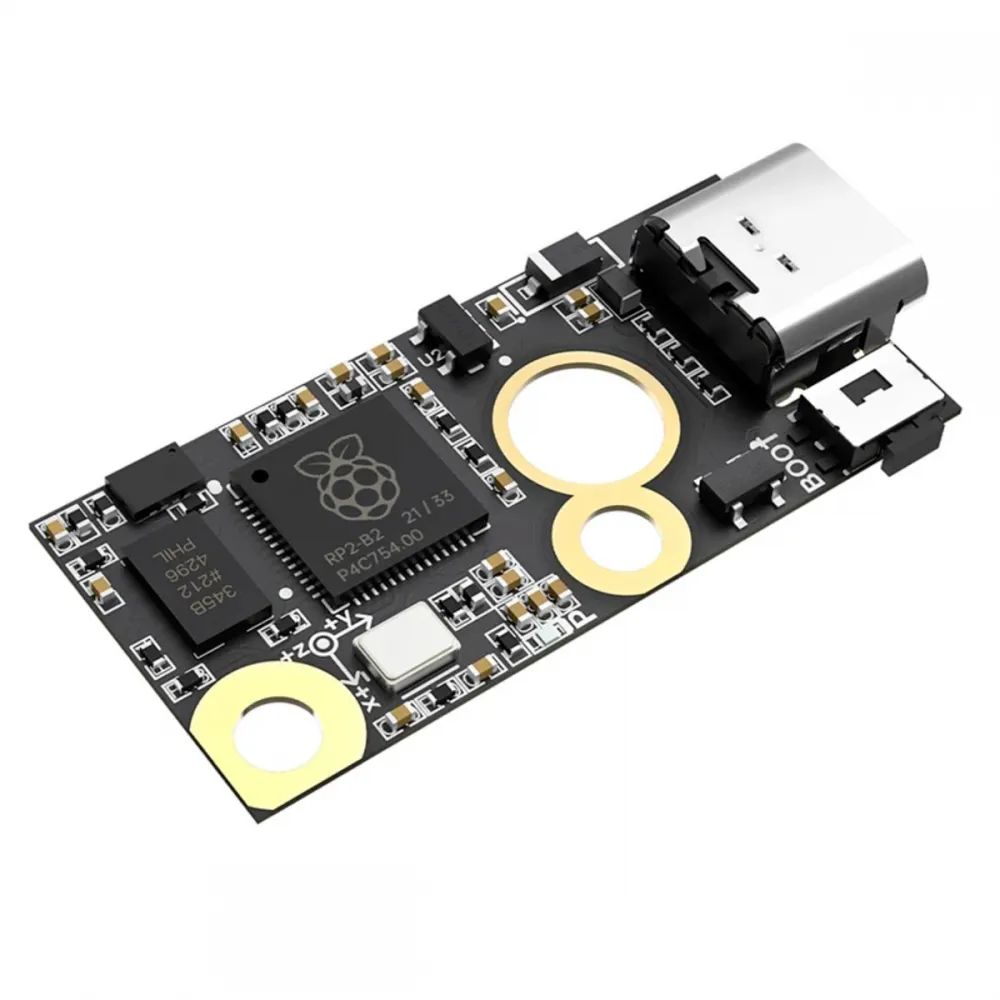
The BIGTREETECH ADXL345 V2.0 is a USB accelerometer designed to measure a 3D printer's resonances and help calibrate Input Shaper in Klipper. It combines an ADXL345 sensor with its own RP2040 microcontroller, allowing it to connect to the Klipper host over USB-C without routing SPI signals to the main controller board.
The module records the machine's mechanical response; Klipper then analyses the data and proposes the compensation parameters. This enables measured Input Shaper tuning, but it does not replace checking belts, pulleys, bearings, fasteners, frame rigidity or moving masses.
What this USB version offers
- Direct host connection: the RP2040 operates as a secondary Klipper MCU and sends ADXL345 measurements over USB.
- Local hardware SPI: the sensor communicates with the on-board RP2040, avoiding a long, noise-sensitive SPI harness.
- Reusable installation: it can be mounted temporarily to calibrate several machines and removed afterwards.
- Straightforward updating: a BOOT button provides DFU access, while reserved solder pads support custom wiring.
- USB protection: BIGTREETECH includes additional ESD protection on the port.
| Feature | Specification |
|---|---|
| Model | BIGTREETECH ADXL345 V2.0 |
| Microcontroller | RP2040, dual ARM Cortex-M0+ up to 133 MHz |
| Accelerometer | ADXL345 |
| Internal communication | Four-wire SPI |
| Host connection | USB 2.0 through USB-C |
| Power | 5 V DC over USB; 3.3 V internal logic |
| Published resolution | Up to 3.9 mg/LSB |
| Output data rate | 0.1–3200 Hz |
| Sensor temperature range | −40 to +85 °C |
| Dimensions | 33.25 × 15.5 mm |
| Firmware | Klipper |
Actual compatibility
It can be used with a Raspberry Pi, CB1/BTT Pi or another Linux Klipper host provided that it has a working USB port, recognises the RP2040 MCU and can run the dependencies required for resonance analysis. Because communication is handled by the host, a BIGTREETECH controller board or dedicated ADXL connector is not required.
Compatibility is not completely automatic: the correct RP2040 firmware must be built or installed, its USB path identified, the configuration added, the sensor orientation defined and a safe test point chosen for the actual machine.
BIGTREETECH currently documents this product for Klipper. It is not presented as a direct calibration module for Marlin or RepRapFirmware.
Mounting for different kinematics
- CoreXY, Voron and machines with a stationary XY bed: one rigid toolhead mount can measure both X and Y.
- Cartesian bed-slingers: Klipper recommends measuring X with the accelerometer on the toolhead and Y with it attached to the bed. The same unit can be moved between the two tests.
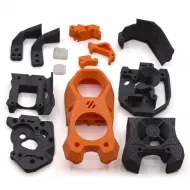
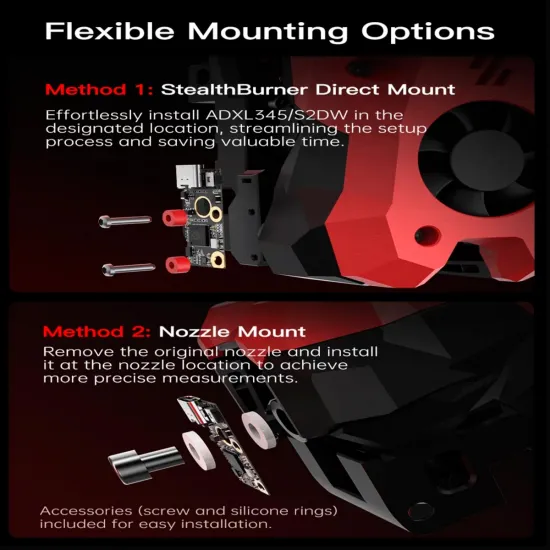
- StealthBurner: BIGTREETECH provides for side mounting through the two mounting points on the assembly.
- Nozzle position: the screw and silicone rings support a temporary installation close to the nozzle, always with the hotend cold and unpowered.
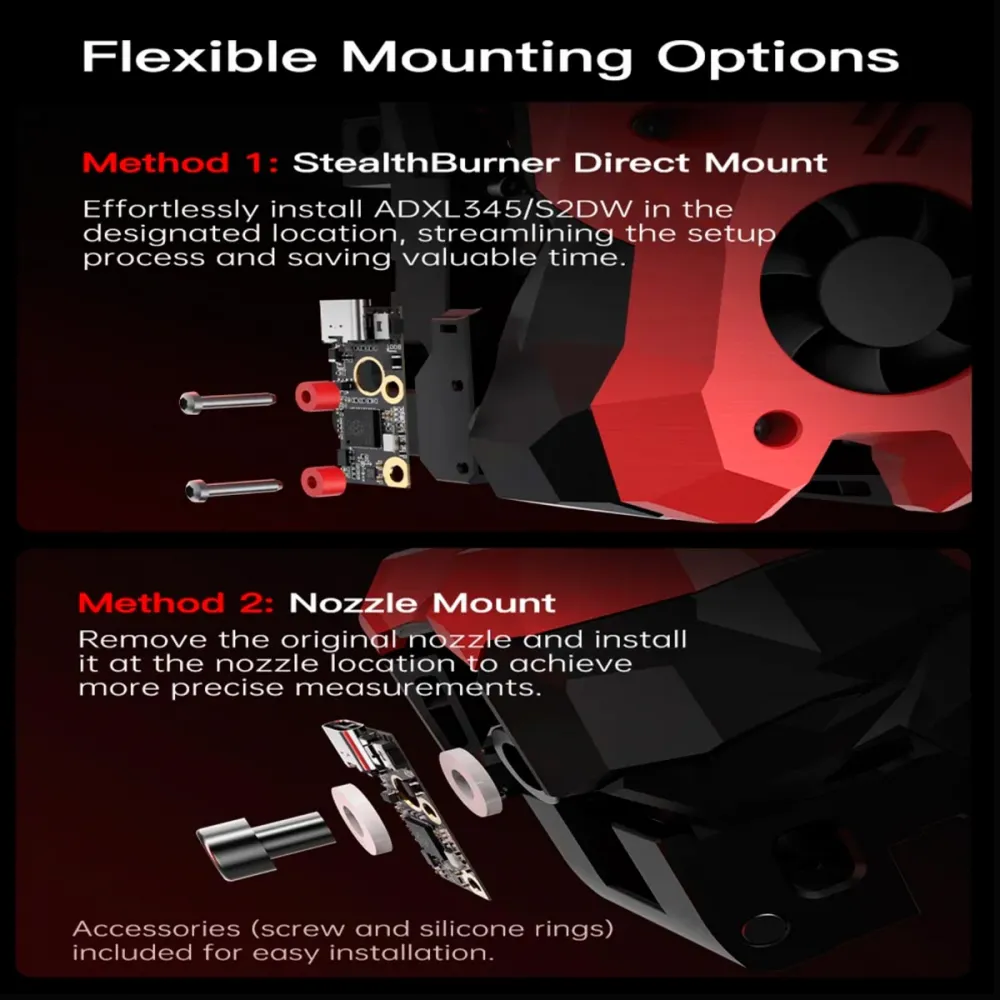
The sensor must be rigidly attached to the component being measured. A flexible bracket, loose screws or a USB cable pulling on the PCB can distort the result. Also prevent the PCB or mounting screws from creating an unintended electrical connection to metal printer parts.
Building Klipper firmware for the RP2040
The May 2025 official manual specifies the following make menuconfig basis:
- Enable extra low-level configuration options: enabled.
- Micro-controller Architecture: Raspberry Pi RP2040/RP235x.
- Processor model: rp2040.
- Bootloader offset: No bootloader.
- Flash chip: GENERIC_03H with CLKDIV 4.
- Communication interface: USBserial.
cd ~/klipper
make clean
make menuconfig
make
To enter DFU, hold BOOT while connecting USB-C to the host. Check the detected device with lsusb and use its actual identifier when flashing:
lsusb
cd ~/klipper
make flash FLASH_DEVICE=2e8a:0003
ls /dev/serial/by-id/*
2e8a:0003 is the common DFU identifier shown in the documentation, not a value to assume if lsusb reports another one. The path found under /dev/serial/by-id/ is the one to place in the configuration.
Current Klipper configuration
BIGTREETECH's current example uses the RP2040 hardware SPI bus. Create a separate file such as btt-adxl345.cfg and adapt at least the serial, orientation and test point:
[mcu btt_adxl345]
serial: /dev/serial/by-id/ACTUAL_MODULE_USB_ID

[adxl345]
cs_pin: btt_adxl345:gpio9
spi_bus: spi1_gpio8_gpio11_gpio10
axes_map: -x,-y,-z

[resonance_tester]
accel_chip: adxl345
probe_points:
    100, 100, 20
Then include the file from printer.cfg:
[include btt-adxl345.cfg]axes_map: -x,-y,-z matches the orientation in the official example. It must describe how the axes printed on the PCB relate to the printer axes. The 100, 100, 20 point is also only an example and must be within the real travel, slightly above a central area and clear of obstacles.Checking and calibrating Input Shaper
- With the machine stationary, restart Klipper and run
ACCELEROMETER_QUERY. It should return plausible acceleration values. - Run
MEASURE_AXES_NOISE. Very high noise should prompt checks of the mount, power, wiring, sensor and fans before calibration. - Check that belts, pulleys, screws, toolhead, bed and frame are correctly adjusted.
- Supervise the first test and keep
M112ready: the sweep generates intense vibration. - Run
SHAPER_CALIBRATE AXIS=Xfollowed bySHAPER_CALIBRATE AXIS=Y. On a bed-slinger, move the sensor to the corresponding component between tests. - Review Klipper's recommendations and run
SAVE_CONFIGonly when they are sensible. - Validate the result with actual prints and set a suitable maximum acceleration separately;
SAVE_CONFIGdoes not automatically choose a safemax_accel.
Recalibrating before every print is not recommended. Klipper warns that repeatedly running these intensive tests may increase wear or loosen components. Recalibrate after relevant mechanical changes and inspect the machine after each test.
[include btt-adxl345.cfg] before restarting. Otherwise Klipper will wait for a USB MCU that is no longer connected and will be unable to complete startup.ADXL345 V2.0 or S2DW V1.0
Both BIGTREETECH modules target the same application and combine an RP2040 with USB, but they use different sensors and configuration sections. This model contains an ADXL345, which is widely supported by Klipper. The BIGTREETECH S2DW V1.0 with LIS2DW sensor is also available. Do not interchange their configuration files merely because the boards have a similar format.
It is for you if
- You use Klipper and want to calibrate Input Shaper from real measurements.
- You prefer an independent USB connection over routing SPI signals to the main board.
- You can prepare a rigid mount and adapt the serial, orientation and coordinates to your machine.
- You want a reusable tool for diagnosing mechanical changes across several printers.
It is not for you if
- You expect an automatic improvement without configuring firmware or running tests.
- Your printer does not use Klipper, or the host cannot support the USB MCU and analysis dependencies.
- You cannot secure the accelerometer rigidly and safely to the toolhead or bed.
- You expect software to repair backlash, loose belts or damaged components.
Contents
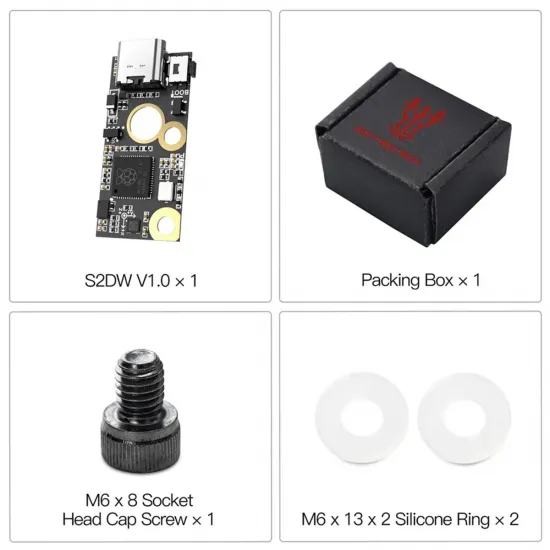
- 1 × BIGTREETECH ADXL345 V2.0 module.
- Screw and silicone rings for the temporary mounting method shown by BIGTREETECH.
See the official BIGTREETECH ADXL345 repository for the manual, dimensional drawing, STEP model and current configuration file. Follow Klipper's official Measuring Resonances documentation for the test procedure and software requirements.