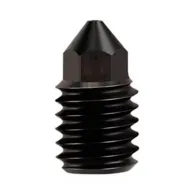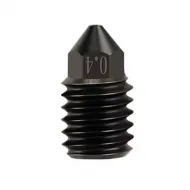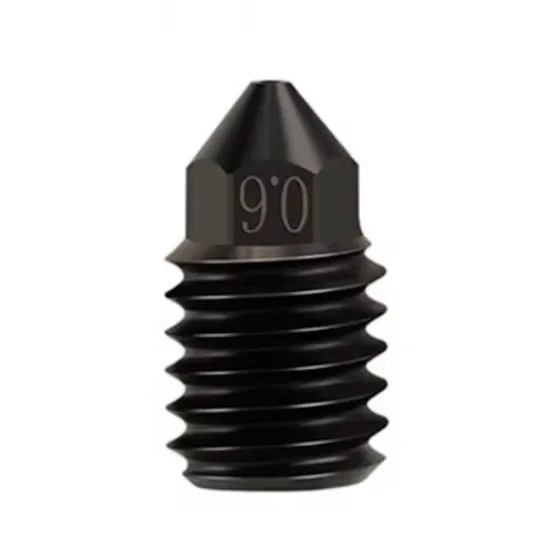
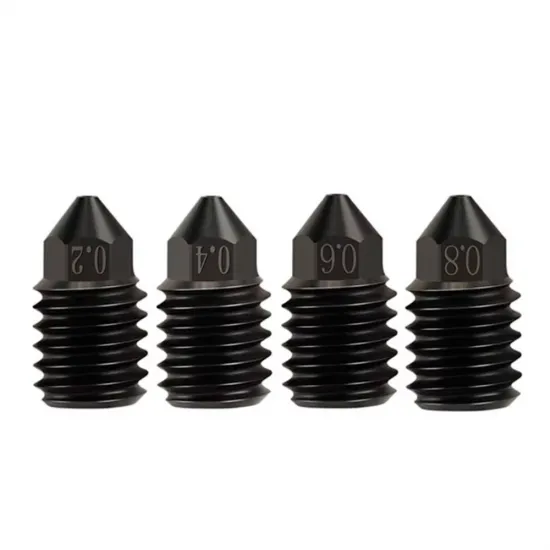
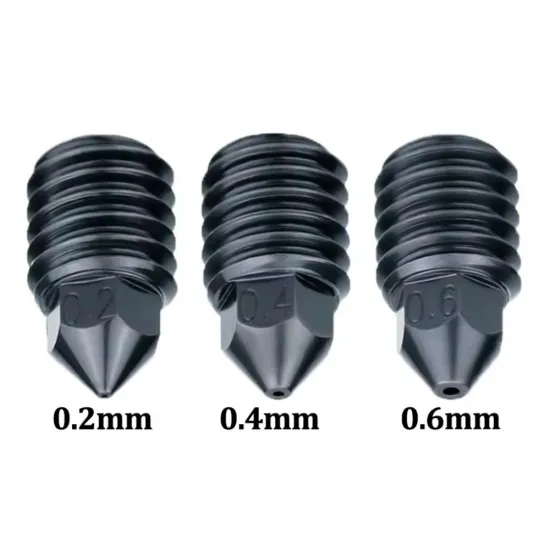


- Stock: 12
- Model: Nozzle-TZ-V6-0.6

Diameter

0.3mm

0.4mm

0.6mm
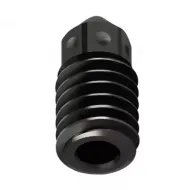
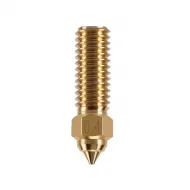
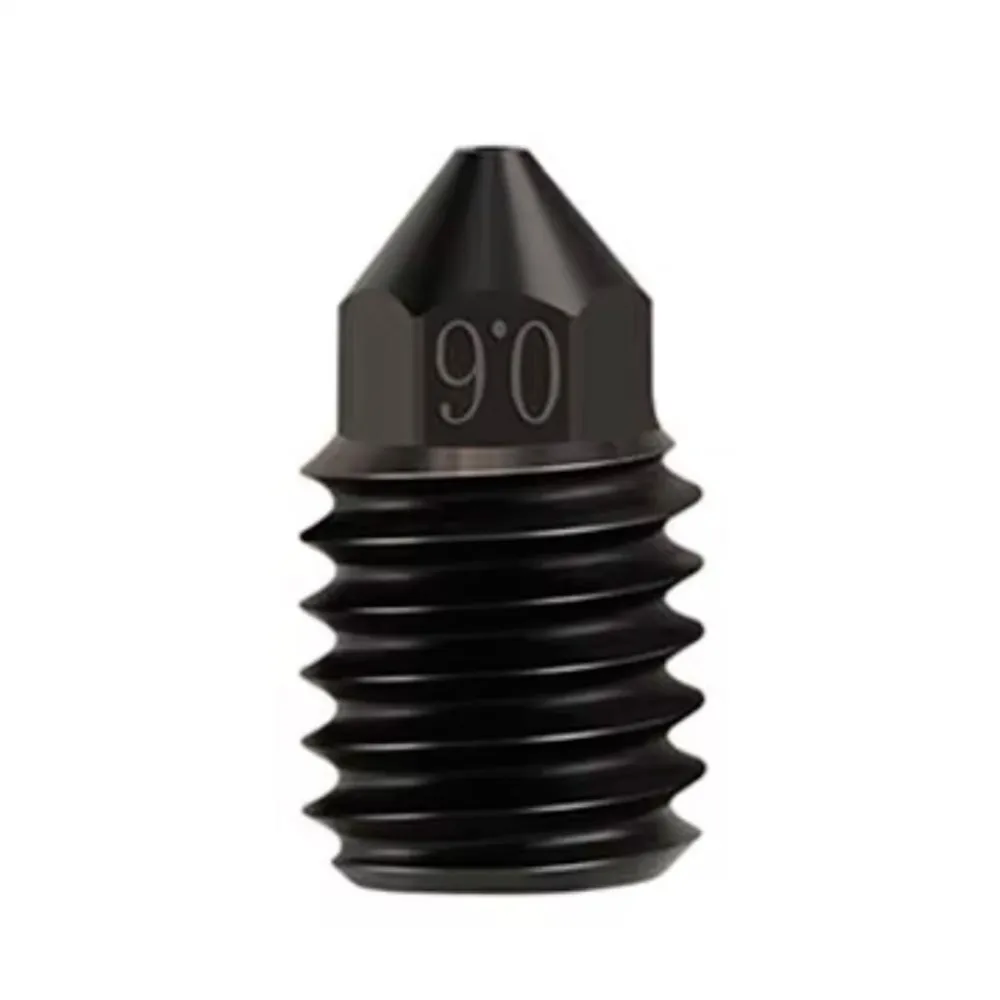
0.6 mm nozzle for the TZ-V6 2.0 hotend, manufactured from hardened SKD11 steel with a DLC surface treatment. Its larger outlet supports wider lines and thicker layers while providing more clogging margin with many filled filaments.
Main features
- Nominal outlet: 0.6 mm.
- Filament: 1.75 mm.
- Material: hardened SKD11 steel with DLC treatment.
- Stated hardness: HRC 60+.
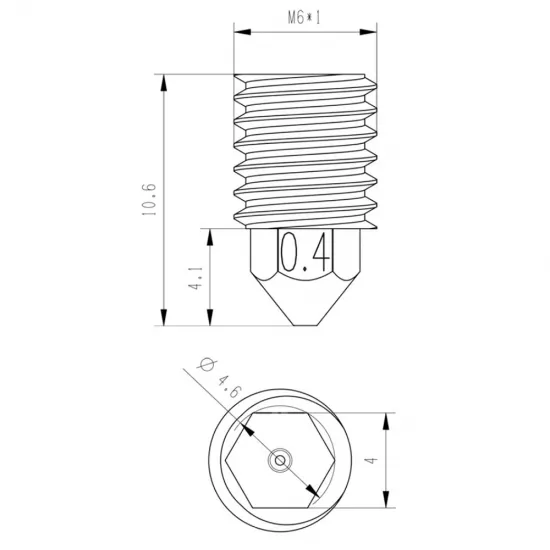
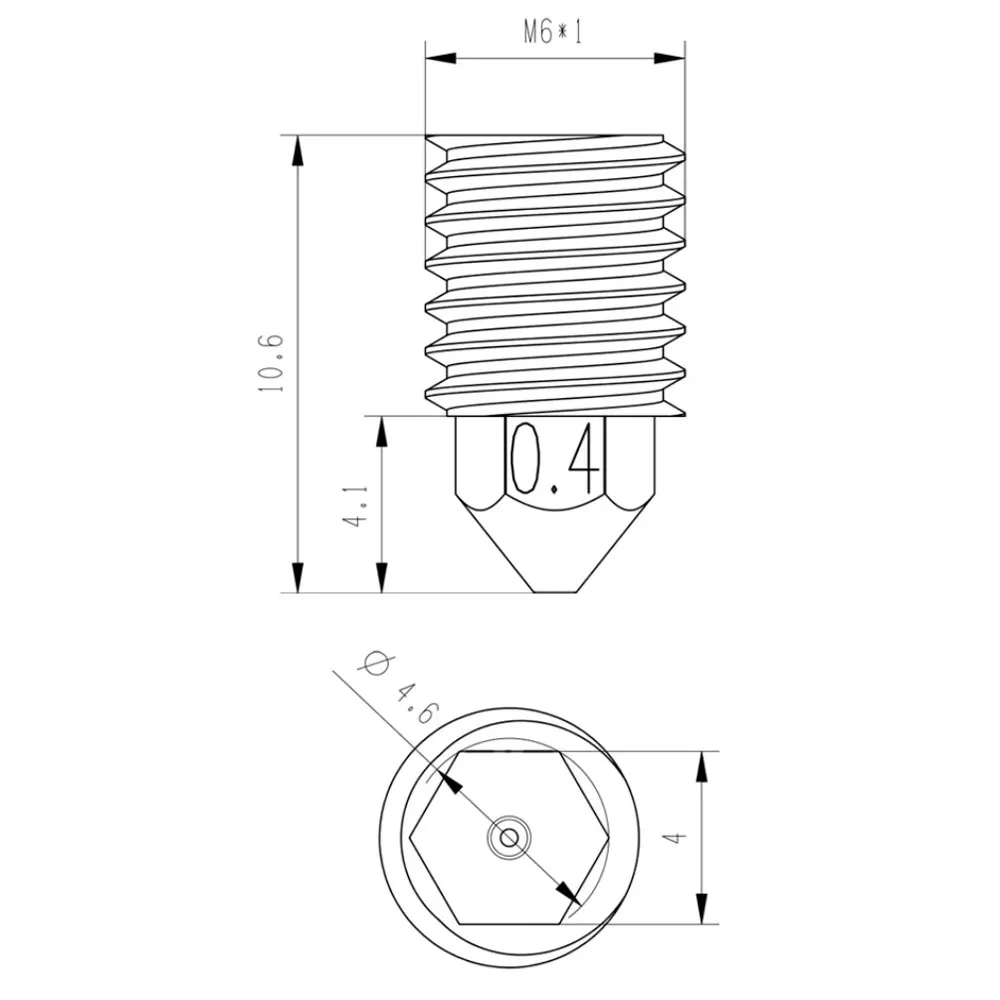
- Thread: M6 × 1.
- Overall length: 10.6 mm.
- Hex: 4 mm across flats.
- Flow path: one central outlet; not a three-channel CHT nozzle.
Compatibility and dimensions
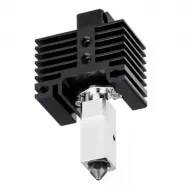
This is a dedicated replacement for the TZ-V6 2.0 hotend and assemblies using exactly the same geometry. An M6 × 1 thread does not make it universal: length, threaded depth, sealing seat, spanner access and final height must all match.
| Nominal dimension | Value |
|---|---|
| Thread | M6 × 1 |
| Overall length | 10.6 mm |
| Lower section | 4.1 mm |
| Hex | 4 mm across flats |
The drawing uses the 0.4 mm version as its geometric reference; this nozzle shares the outer dimensions and changes the nominal outlet to 0.6 mm.
Why choose 0.6 mm
It suits functional parts, wide perimeters and thicker layers. Approximate 0.15 to 0.48 mm layers are a useful starting range, subject to part geometry, material and slicer.
It provides more clearance for carbon-fibre, glass-fibre, wood, metal, glow-pigment and other filled filaments, but the material manufacturer's minimum diameter must still be observed. A larger hole alone cannot guarantee clog-free printing with every compound.
This is for you if
- You have a TZ-V6 2.0 and prioritise throughput or functional parts.
- You print abrasive materials that recommend 0.6 mm.
- You want thicker layers and lines and accept reduced small-feature detail.
This is not for you if
- Your hotend uses a different nozzle geometry.
- You require very small details, fine lettering or narrow walls.
- Your hotend or extruder cannot sustain the required volumetric flow.
Installation and calibration
- Follow the installed TZ-V6 procedure and do not apply a universal temperature or torque.
- Hold the block stationary and use a 4 mm spanner, avoiding loads on the heatbreak and contact with wiring.
- Check the seal and inspect for leaks at operating temperature.
- Set 0.6 mm in the slicer and verify that Klipper's
nozzle_diametermatches the installed part. - Recalibrate the first layer or Z offset, temperature, flow, retraction, Pressure Advance or Linear Advance and maximum volumetric flow.
A 0.6 mm nozzle may demand more material per second than 0.4 mm. Increasing line width or layer height without checking melt capacity can cause under-extrusion. The complete TZ-V6 2.0 is published for operation up to 300 °C; the lowest thermal limit in the assembly always prevails.
For finer detail, see the 0.3 mm and 0.4 mm versions, plus the TZ-V6 silicone sock.
Package contents
1 hardened-steel TZ-V6 nozzle with a 0.6 mm outlet. Hotend and tools are not included.