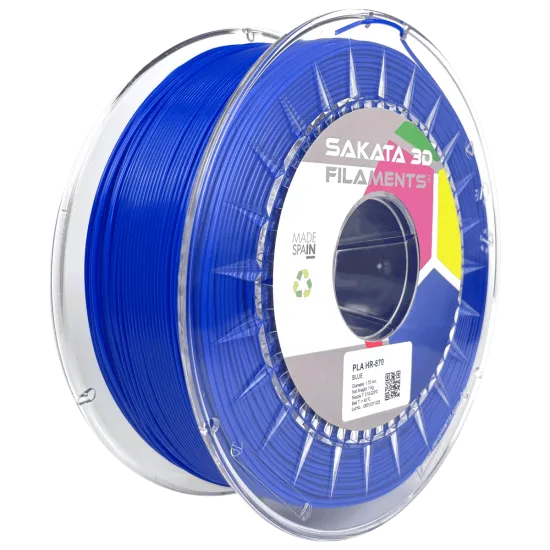
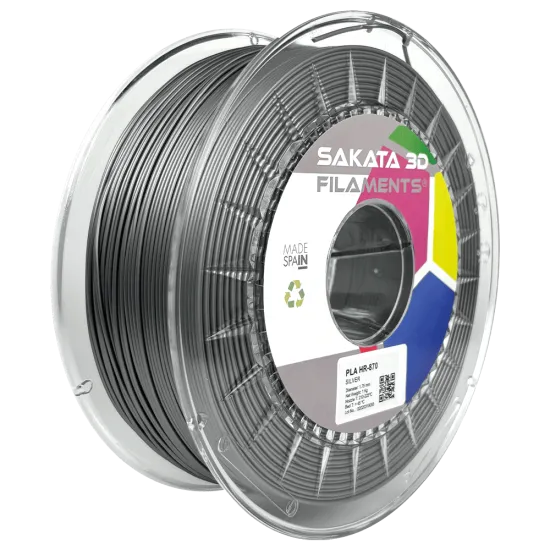
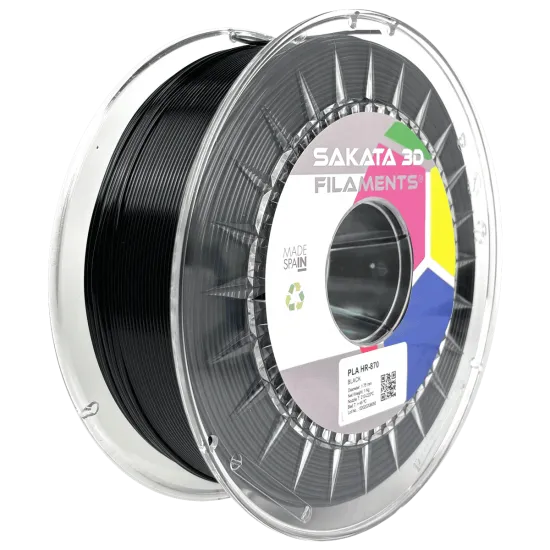


- Stock: 157
- Model: PLA-3D870-1.75mm-SAKATA3D

Type:

PLA GO&PRINT

GO&PRINT Transition

GO&PRINT Recycled

PLA-M

PLA-M Transition

PLA 3D850

PLA INGEO 3D850 Fluor

PLA 3D850 MAGIC / MAGIC+

PLA 3D850 SILK

PLA 3D850 GLASS

PLA 3D850 Transition

3D850 Recycled

HR-PLA 3D870

HR-PLA 3D870 Transition

Recycled 3D870

PLA High Speed

PLA High Speed PRO

PLA High Speed PRO TransitionHigh Speed
Sakata 3D PLA HR-870 is a Spanish-made engineering filament based on Ingeo 3D870, formulated to improve impact resistance and thermal performance over conventional PLA. It retains PLA's accessible printing behaviour and supports both conventional and high-flow printer profiles.
What HR-870 offers
- Greater impact resistance and potential thermal performance than standard PLA.
- Low warping tendency and good detail reproduction.
- Conventional and high-speed profiles documented by Sakata 3D.
- Non-abrasive material suitable for a conventional Brass nozzle.
- Made in Spain by Sakata 3D Filaments.
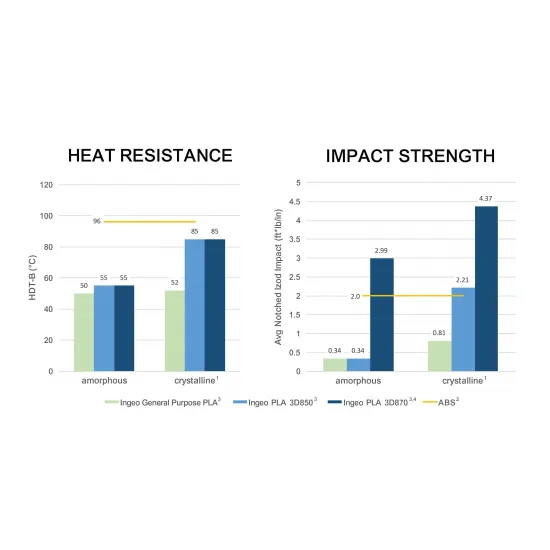
The manufacturer compares selected properties with ABS, but this is not a universal drop-in replacement claim. Final strength depends on orientation, geometry, walls, infill, inter-layer bonding, moisture, profile and heat treatment.
Specifications
| Property | Value |
|---|---|
| Material | Modified Sakata 3D HR-870 PLA based on Ingeo 3D870 |
| Diameter | 1.75 ± 0.03 mm |
| Maximum roundness deviation | 0.03 mm |
| Net weight | 1 kg |
| Declared density | 1.22 g/cm³ |
| Recommended nozzle | Brass; 0.4 mm reference |
| Enclosed chamber | Not required |
| Origin | Made in Spain |
Print settings
Official starting values for a 0.4 mm nozzle. Tune temperature, retraction, flow and cooling with a test on your printer.
| Setting | Conventional printing | High speed |
|---|---|---|
| Nozzle temperature | 210–225 °C | 225–240 °C |
| Speed | 50–100 mm/s | 100–400 mm/s |
| Declared maximum volumetric flow | Tune for the hotend | 32 mm³/s at 240 °C |
| Bed | Above 45 °C; glass or PEI; adhesive if required | |
| Part-cooling fan | 100% | |
| Layer height | From 0.1 mm | |
400 mm/s is not guaranteed for every print. The practical limit depends on hotend flow, nozzle, line width and layer height, geometry, extruder, acceleration and cooling. When mechanical performance matters, prioritise stable extrusion and strong layer bonding over headline speed.
Annealing and thermal performance
Sakata states a 75–85 °C HDT at 0.45 MPa for 100%-infill printed specimens crystallised at 110 °C for 20 minutes. This is not a guaranteed service temperature for every printed part. Orientation, cross-section, load and process affect the result.
Annealing can improve heat stability but may cause shrinkage, warping or dimensional change. For critical parts, print and measure a representative specimen, apply a controlled thermal cycle, allow it to cool and measure it again. Large or thin parts may require support during treatment.
Drying and storage
Drying is optional. If popping, bubbles, stringing or a rough surface appear, Sakata recommends 4–6 hours at 55 °C; feeding from a dryer at 55 °C is also supported. Store the spool sealed with desiccant and ensure the dryer controls temperature accurately.
3D-printer compatibility
It is functionally compatible with FDM/FFF printers for 1.75 mm filament that can reach the stated temperature range. With a tuned profile it can be used on HTA3D HPRO machines and families such as Bambu Lab A1, P1 and X1; Creality Ender-3 and K1; Original Prusa MK3, MK4, MINI and CORE One; and Voron 0.2, Trident or 2.4 builds.
AMS, MMU, CFS and other automatic-feeder compatibility must be checked for spool condition, path and friction; it is not universally guaranteed.
This product is for you if
- You want easy-to-print PLA with scope for improved impact and thermal performance.
- You need both conventional and high-flow profiles.
- You can validate or anneal parts for demanding applications.
This product is not for you if
- You need certified service temperature or strength without testing the final part.
- You need a universal drop-in ABS substitute.
- The application requires food-contact or medical certification.
You can also choose Sakata 3D RE-HR870 recycled filament or Sakata 3D HR-870 transition-colour filament.
Printing in a space with suitable general ventilation is recommended.