

- Stock: 41
- Model: PLA-M-1.75mm-SAKATA3D

Type:

PLA GO&PRINT

GO&PRINT Transition

GO&PRINT Recycled

PLA-M

PLA-M Transition

PLA 3D850

PLA INGEO 3D850 Fluor

PLA 3D850 MAGIC / MAGIC+

PLA 3D850 SILK

PLA 3D850 GLASS

PLA 3D850 Transition

3D850 Recycled

HR-PLA 3D870

HR-PLA 3D870 Transition

Recycled 3D870

PLA High Speed

PLA High Speed PRO

PLA High Speed PRO TransitionHigh Speed
Sakata 3D PLA-M is a PLA filament made in Spain and formulated to produce parts with a matte finish and reduced layer-line visibility. Its low-gloss surface helps soften the visual transition between layers and gives figures, scale models, enclosures, decorative objects and presentation prototypes a particularly uniform appearance.
Although its texture has a slightly rough appearance, the manufacturer classifies it as non-abrasive: it can be printed with a conventional Brass nozzle. The formulation combines easy printing with a dedicated high-speed range, provided that the hotend and motion system can supply the required flow.
Why choose PLA-M
- Matte, very low-gloss surface.
- Visually reduces the appearance of print lines, although it cannot hide calibration defects.
- Reliable adhesion and low shrinkage from an easy-to-use PLA formulation.
- Supports conventional and high-speed print profiles.
- Non-abrasive: no hardened nozzle is required.
- Made in Spain by Sakata 3D Filaments.
Specifications and presentation
| Property | Value |
|---|---|
| Material | Matte-finish PLA |
| Diameter | 1.75 ± 0.03 mm |
| Maximum roundness deviation | 0.03 mm |
| Net weight | 1 kg |
| Nominal spool dimensions | Ø195 × 70 mm; Ø53 mm hub |
| Packaging | Vacuum-sealed bag with desiccant |
| Origin | Made in Spain |
Available colours
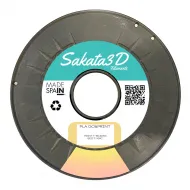
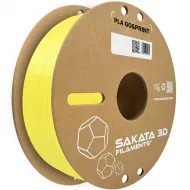
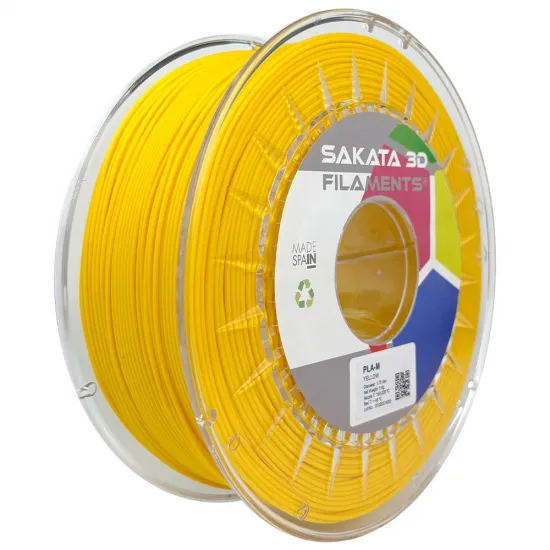
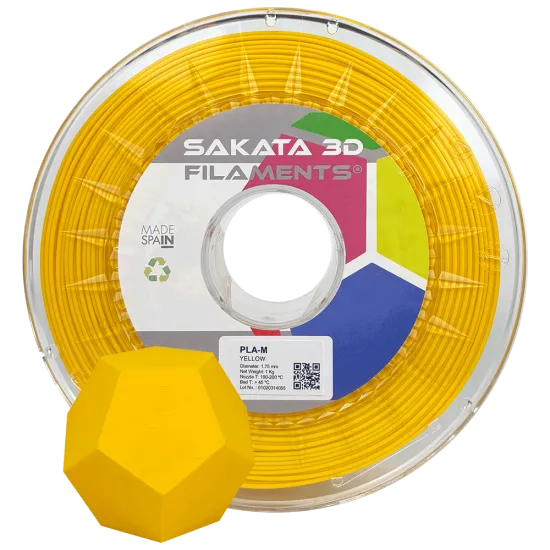
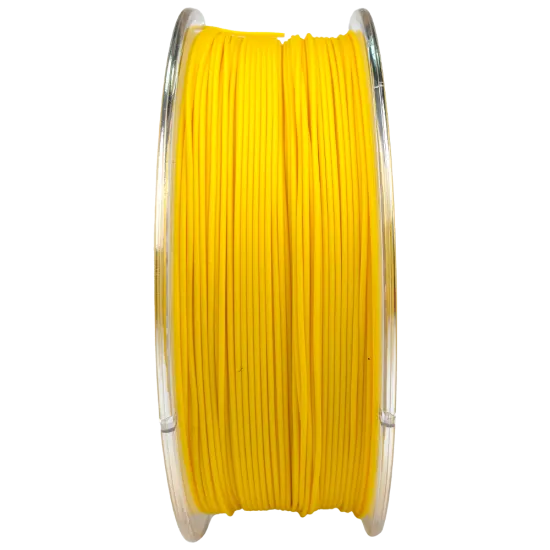
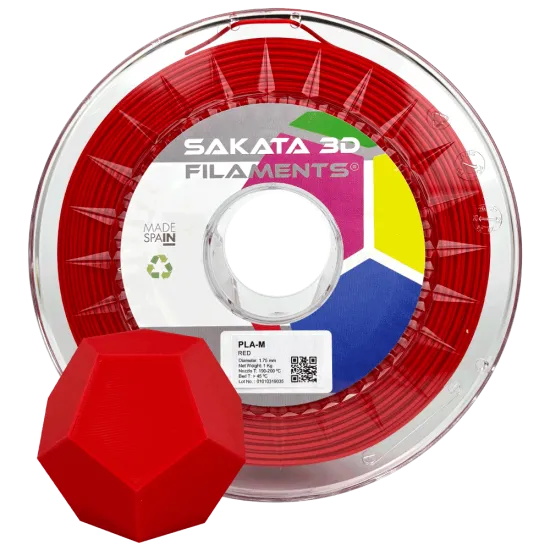
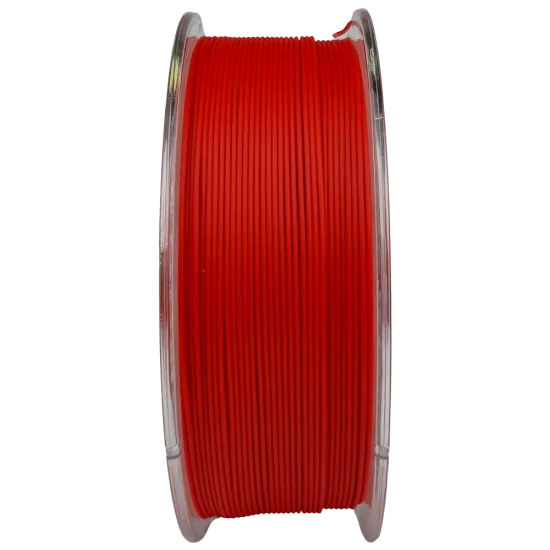
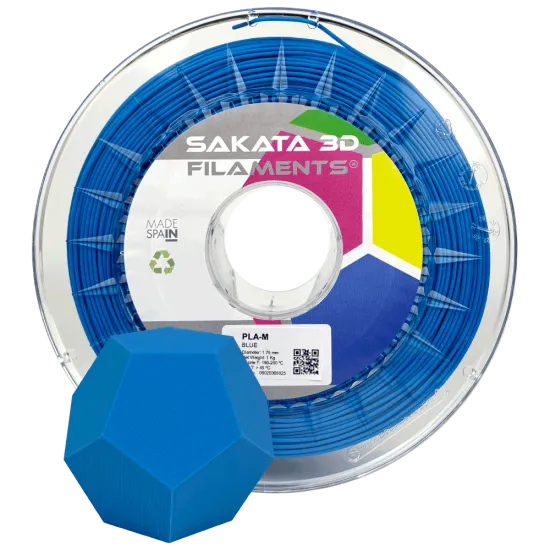
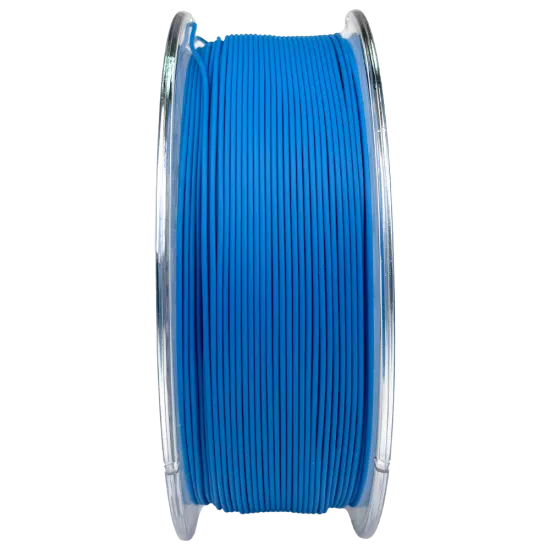
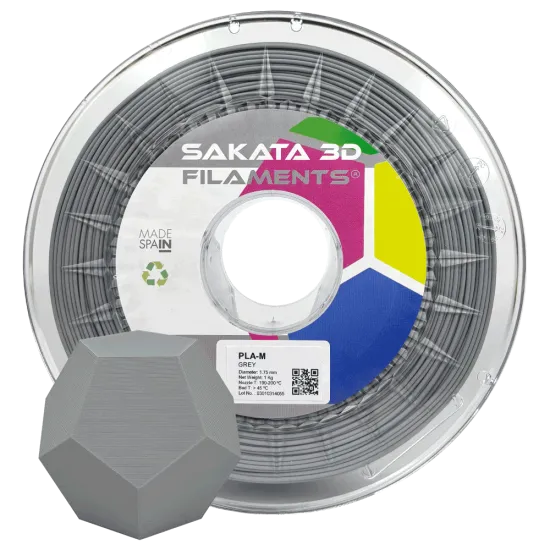
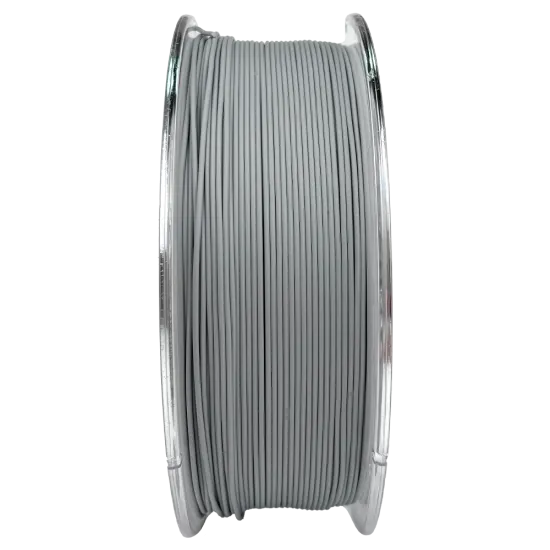
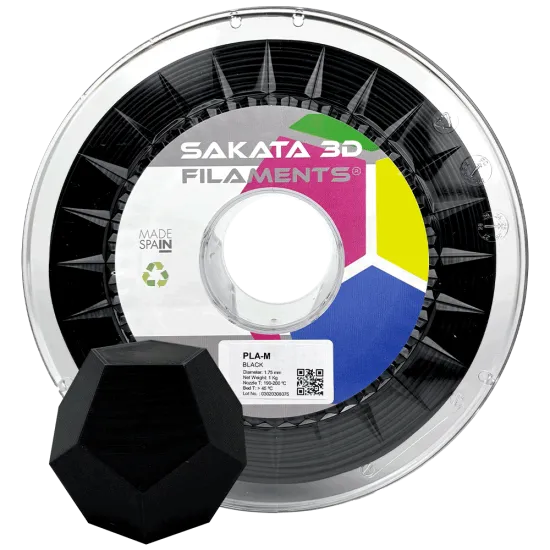
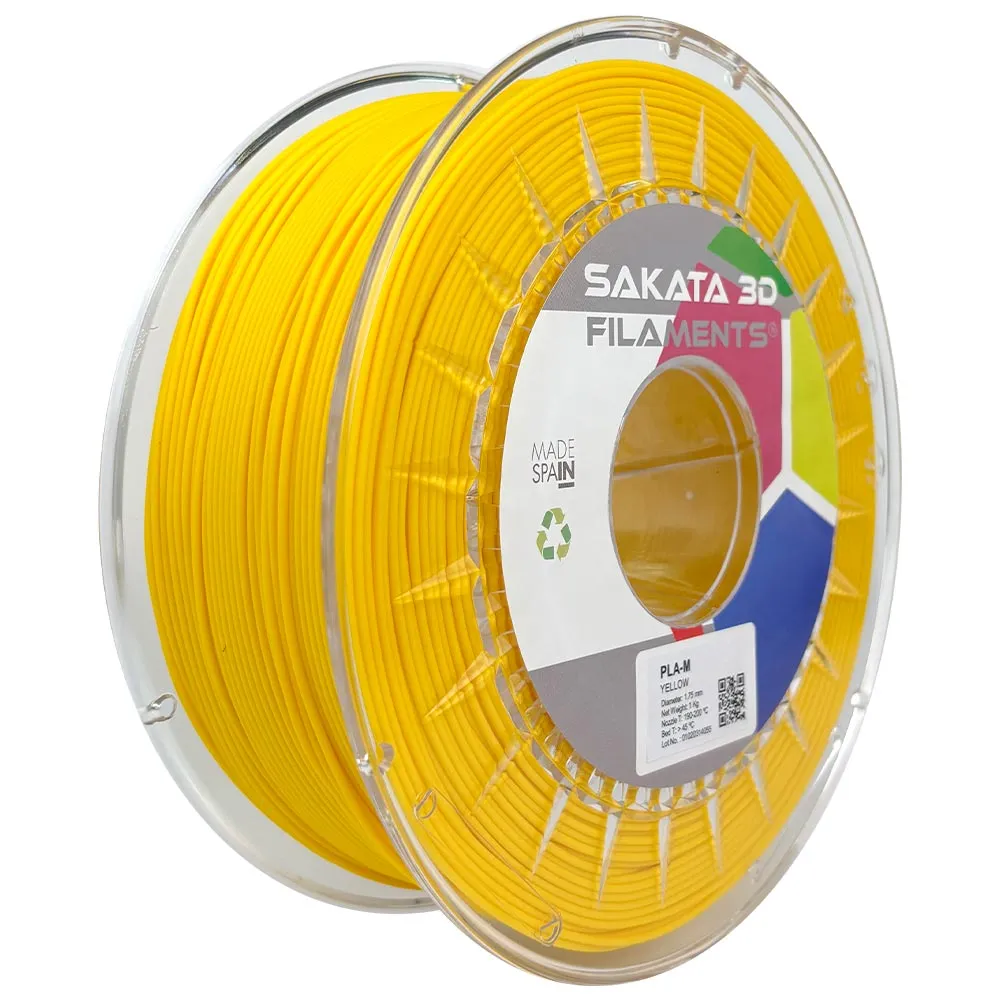
Choose from White, Yellow, Red, Blue, Grey or Black. The photograph shows the yellow presentation; the perceived shade may vary slightly with lighting, screen calibration, production batch and print settings.
Print settings
The current Sakata 3D technical data sheet distinguishes conventional and high-speed printing. Values are based on a 0.4 mm nozzle and should be used as a starting point for calibrating each machine.
| Setting | Conventional printing | High speed |
|---|---|---|
| Nozzle temperature | 190-200 °C | 200-240 °C |
| Print speed | 50-120 mm/s | 120-480 mm/s |
| Declared maximum volumetric flow | Calibrate for the hotend | 33 mm³/s at 240 °C |
| Bed | Above 45 °C; glass or PEI | |
| Part-cooling fan | 100% | |
| Layer height | 0.1-0.3 mm | |
| Nozzle | 0.4 mm Brass reference; hardened steel is not required | |
For a reliable starting profile, begin in the conventional range and tune temperature, flow, retraction and cooling with a small test. Increase speed only after confirming that the hotend maintains stable flow and that the layers remain properly bonded.
Drying and storage
Drying is optional, but it may help if popping, bubbles, stringing, a rough surface or unstable extrusion appear. Sakata 3D specifies 2-4 hours at 60 °C before printing and allows the filament to be held at 60 °C while printing.
After opening the bag, store the spool sealed with desiccant. Make sure the dryer controls temperature correctly and that the spool can withstand the cycle without deformation.
3D printer compatibility
It is functionally compatible with FDM/FFF printers designed for 1.75 mm filament and capable of operating within the selected temperature range. With a properly tuned profile, this includes HTA3D HPRO machines and popular families such as Bambu Lab A1, A1 mini, P1P, P1S and X1 Carbon; Creality Ender-3, CR-10, K1, K1C and K1 Max; Original Prusa MK3, MK4, MINI and CORE One; and Voron 0.2, Trident or 2.4 configurations.
Compatibility does not imply a universal profile. Hotend, extruder, nozzle, build surface and enclosure revisions affect results. On enclosed printers, follow the machine manufacturer's recommendation for chamber ventilation when printing PLA.
Material properties
The technical data sheet states a density of 1.32 g/cm³ and an HDT of 55 °C at 0.45 MPa. The latter is measured on injection-moulded specimens and is not a guaranteed service temperature for a printed part. Orientation, perimeters, infill, layer bonding and load conditions significantly affect final performance.
As with any PLA, it is not the first choice for parts exposed to high heat, prolonged outdoor use or severe impact without application-specific validation. It is not certified for food contact or medical applications.
This product is for you if
- You want a uniform matte finish with visually subdued layer lines.
- You print figures, scale models, decorations, cosplay parts, enclosures or presentation prototypes.
- You want an easy-to-print Spanish PLA that can also be used with faster profiles.
This product is not for you if
- You need gloss, a silk effect or transparency.
- The part will be exposed to temperatures near or above the usual range for PLA.
- You require food-contact or medical certification, or guaranteed structural properties in the printed part.
For the same aesthetic with random colour changes, choose Sakata 3D PLA-M transition-colour filament. If extreme print speed is the priority, consider Sakata 3D PLA High Speed PRO; for the specific properties of NatureWorks Ingeo 3D850, choose Sakata 3D PLA Ingeo 3D850.
Printing in a space with suitable general ventilation is recommended.