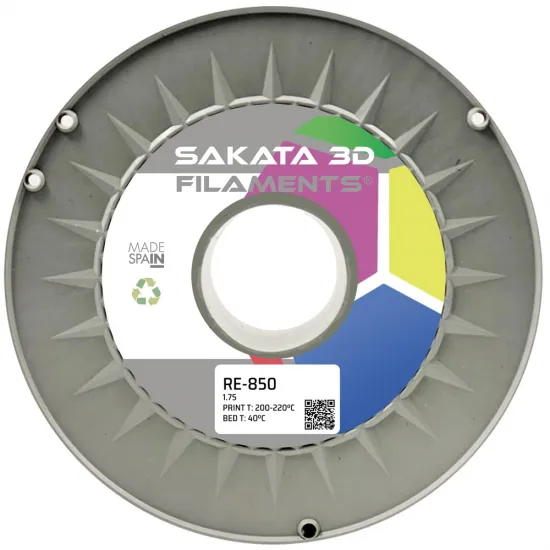
- Stock: 55
- Model: PLA-3D850-1.75mm-SAKATA3D

Type:

PLA GO&PRINT

GO&PRINT Transition

GO&PRINT Recycled

PLA-M

PLA-M Transition

PLA 3D850

PLA INGEO 3D850 Fluor

PLA 3D850 MAGIC / MAGIC+

PLA 3D850 SILK

PLA 3D850 GLASS

PLA 3D850 Transition

3D850 Recycled

HR-PLA 3D870

HR-PLA 3D870 Transition

Recycled 3D870

PLA High Speed

PLA High Speed PRO

PLA High Speed PRO TransitionHigh Speed
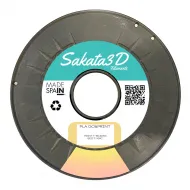
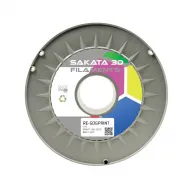
Sakata 3D RE-850 is a filament made in Spain from PLA850 recovered from Sakata's own production process. The manufacturer reuses filament from its production —without adding externally recycled resin— to obtain a material with properties declared as similar to virgin PLA850 while making use of resources that would otherwise remain outside the final product.
It is particularly useful for prototypes, tooling, models, cosplay, fit checks and parts where function matters more than repeating an exact shade. It is supplied as 1.75 mm filament on a 1 kg spool.
Applications
- Dimensional prototypes and assembly tests.
- Tooling, organisers and indoor functional parts.
- Model making, cosplay, draft volumes and parts intended for painting.
- Prints where recovered material is preferred without leaving the PLA850 base family.
Specifications
| Property | Value |
|---|---|
| Material | PLA850 recovered from Sakata's production process |
| Recovered feedstock | Filaments from Sakata's own PLA850 production; no externally recycled resin |
| Diameter | 1.75 ± 0.05 mm |
| Maximum roundness deviation | 0.05 mm |
| Net weight | 1 kg |
| Reference density | 1.24 g/cm³ |
| Colour | Variable with the recovered mixture; may change along a spool and between batches |
| Origin | Made in Spain by Sakata 3D Filaments |
Print settings
The current product-specific manufacturer recommendation is a useful starting point. The technical data sheet allows a wider window, but each printer should be tuned for flow, layer bonding and first-layer performance.
| Setting | Recommended start | Note |
|---|---|---|
| Nozzle | 210-220 °C | Tune within the technical window for the hotend and flow |
| Heated bed | Not mandatory; 40 °C optional | Tune for the surface and first layer |
| Part cooling | Up to 100% | Reduce for initial layers if it harms adhesion |
| Layer height | 0.1-0.3 mm | Subject to nozzle diameter |
| Speed | Printer's PLA profile | The manufacturer publishes up to 120 mm/s; validate actual flow and quality |
For long jobs or multiple parts intended to look alike, check the visible shade at the start of the spool. Colour variation does not necessarily indicate a formulation change or defect: it is an expected consequence of mixing recovered PLA850 in different colours.
Properties and heat resistance
Sakata declares physical, mechanical, chemical and thermal properties similar to virgin PLA850 for RE-850. The data sheet publishes reference figures of 50 MPa tensile strength, 2,315 MPa tensile modulus, 3.31% elongation and 118 J/m notched Izod impact. These are results under specific tests, not guaranteed performance for every FFF geometry, orientation or setup.
The published 80-90 °C HDT applies to 100% infill specimens annealed at 110 °C for 15 minutes. An as-printed part must not automatically be treated as suitable for this range.
Storage
Keep the spool sealed with desiccant. If the filament produces popping, bubbles, stringing or rough surfaces, use a drying cycle suitable for PLA and compatible with the spool. Do not directly copy industrial pellet-drying temperatures.
3D-printer compatibility
It is compatible with open-filament FDM/FFF printers accepting 1.75 mm filament, reaching 210-220 °C and providing part cooling. With a tuned profile it can be used on HTA3D HPRO 330 and HPRO 400; Bambu Lab A1, P1 and X1; Creality Ender-3, CR-10 and K1; Original Prusa MK3, MK4, MINI, XL and CORE One; and Voron 0.2, Trident or 2.4.
These machines are conditional examples, not an approval or universal profile. Check spool holder, filament path, sensor and accepted dimensions before using a multi-spool feeder. On enclosed printers, follow the manufacturer's chamber-ventilation guidance for PLA.
Choose it if
- You print prototypes, tooling, cosplay, models or parts intended for painting.
- You accept colour variation in exchange for using production-recovered PLA850.
- You want a material made in Spain with behaviour close to the PLA850 family.
It is not for you if
- You need to repeat an exact colour across parts, spools or batches.
- A uniform appearance matters more than the variable nature of recovered material.
- The application requires food, medical or guaranteed structural certification.
If you require repeatable solid colours, see standard Sakata 3D PLA 850. Special finishes include PLA 850 Fluor, PLA 850 Silk and translucent PLA 850 GLASS. For complex supports, consider Sakata 3D Easy Off for PLA 850.
Print with suitable general ventilation. The filament is not certified for food-contact or medical applications.