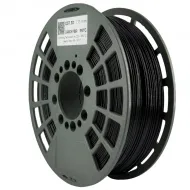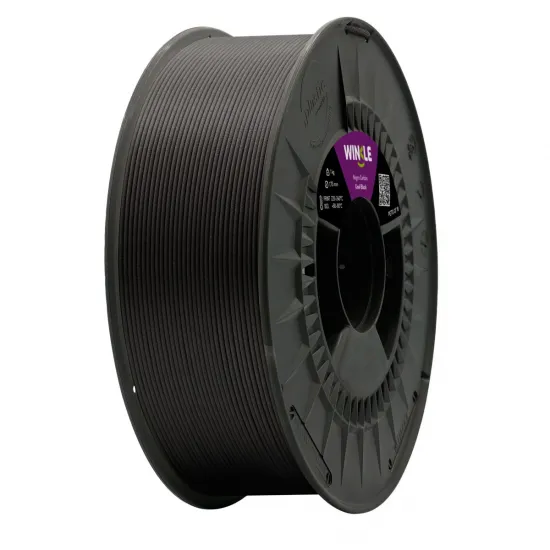


- Stock: 5
- Model: PETG-CF-WINKLE

Colour Range

PETG

KRYSTAL

PETG RE

PETG Carbon Fiber

PETG Prototype

rPETG EN13501-1 Flame Retardant
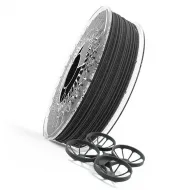
WINKLE 1.75 mm PETG CF is a carbon-fibre reinforced PETG intended for parts requiring higher rigidity, stability and a technical matt-black finish. It is made in Spain and supplied in 300 g and 1 kg spools.
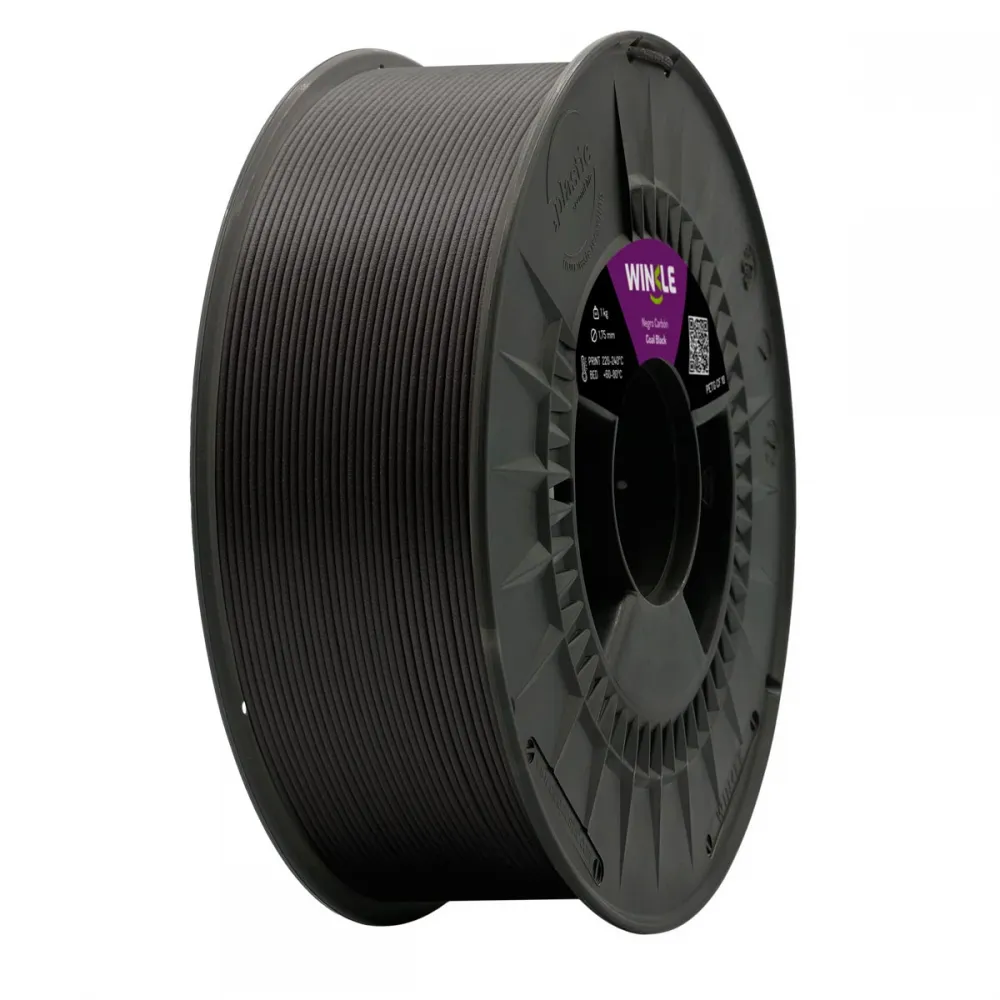
Specifications and starting profile
| Property | Reference |
|---|---|
| Material | Carbon-fibre reinforced PETG |
| Diameter / colour | 1.75 mm / Carbon Black |
| Formats | 300 g and 1 kg |
| Nozzle | 220-260°C |
| Bed | 60-90°C |
| Minimum nozzle | 0.4 mm hardened or wear-resistant |
| Published maximum speed | Up to 150 mm/s, subject to flow and machine |
| Nominal density | 1.23 g/cm³ |
Start at 50-70 mm/s and increase only after checking flow, layer bonding and actual temperature. A 0.6 mm wear-resistant nozzle can reduce clogging risk and provide steadier flow, although WINKLE documents 0.4 mm as the minimum.
What carbon fibre adds
- A matt finish that hides some layer lines.
- Higher rigidity and dimensional stability as formulation goals.
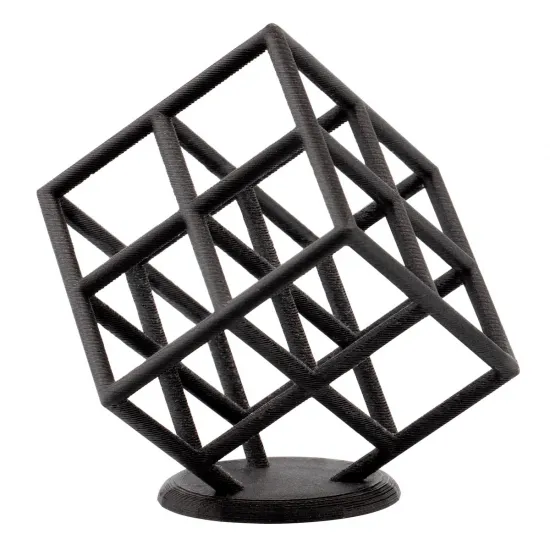
- A useful option for brackets, housings, jigs and technical prototypes.
Rigidity does not mean greater strength in every direction or a certified structural part. The reviewed documentation gives neither a fibre percentage nor a verifiable material-specific mechanical table, so no numerical or universal improvement is claimed.
Printer and feeder compatibility
Requires a 1.75 mm FDM/FFF printer whose hotend reaches the stated range and uses a wear-resistant nozzle. It can be profiled on HTA3D HPRO, Prusa MK3/MK4, Bambu Lab P1/X1, modified Creality Ender 3 and Voron machines when the exact configuration meets those conditions. Filament diameter alone is not enough.
WINKLE lists AMS compatibility, but the fibre is abrasive. Check the feeder manufacturer's guidance, spool compatibility and potential path wear first. Use an external spool holder and a suitable short path if uncertain.
Preparation and maintenance
- Install a wear-resistant nozzle and ensure its actual diameter matches the profile.
- Tune temperature, flow and pressure/advance; do not copy a standard PETG profile without validation.
- Keep sealed and dry with desiccant. Moisture worsens surface, flow and layer bonding.
- Inspect nozzle, gears and tubes after prolonged printing.
- Test orientation and thickness with a representative part before loading it.
If fibre and the matt finish are unnecessary, standard WINKLE PETG reduces wear and simplifies maintenance.
This is for you if
- You want a rigid, black PETG with a technical finish.
- Your machine already has a nozzle and path suitable for abrasive filament.
- You will tune the profile and validate the part under real loads.
This is not for you if
- You only have a brass nozzle and do not want to replace it.
- You need flexibility, translucency or bright colours.
- You need guaranteed structural properties without testing the printed design.