

- Stock: 30
- Model: PLA-PRO-1.75mm

Type:

PLA HD

PLA HD Interference

PLA HD Sweet Pastel

PLA HD With particles

PLA HD GLOW

PLA HD SILK

PLA HD SILK Tricolor

PLA HD Transition

PLA HD Recycled

PLA Ingeo 3D850

PLA Ingeo 3D870

PLA Tough

PLA Matt

PLA High Speed

PLA PRO

PLA UL94 V0
WINKLE PLA PRO: PLA convenience for more demanding parts
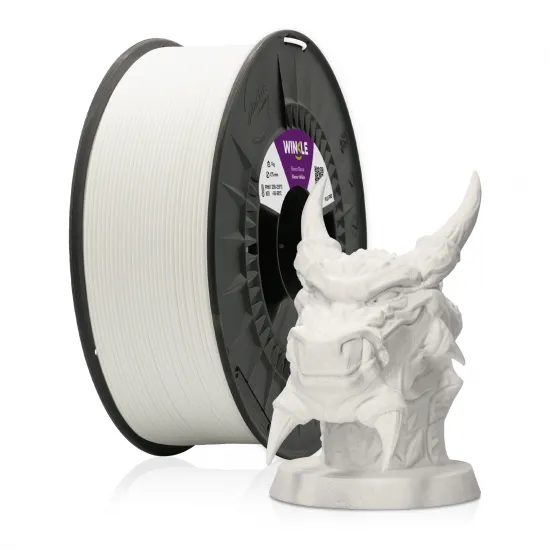
WINKLE PLA PRO 1.75 mm is a filament manufactured in Spain for functional parts, prototypes, tooling and models requiring better thermal and mechanical performance than conventional PLA while remaining relatively easy to print. Its semi-matte finish helps visually soften layer lines and suits both technical components and presentation models.
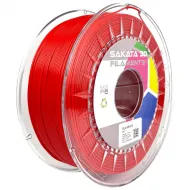
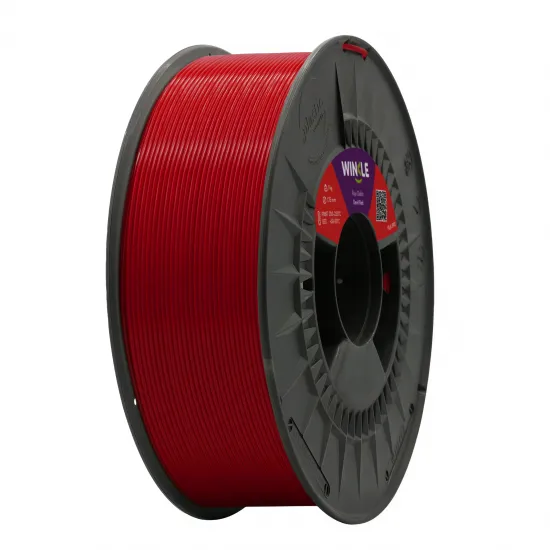
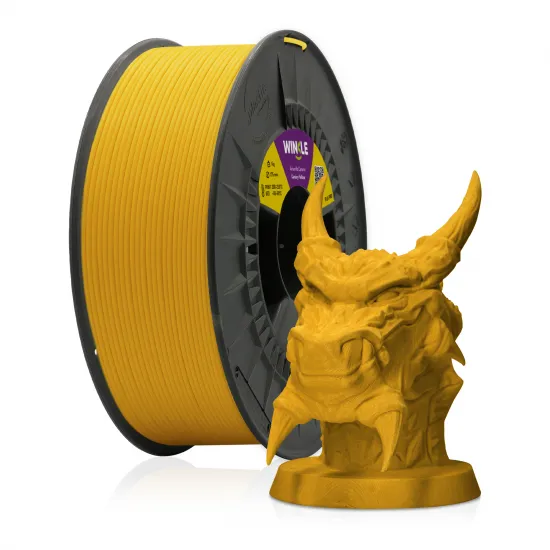
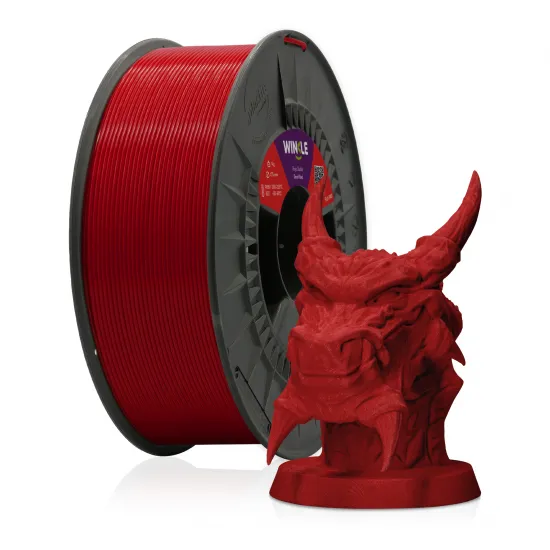
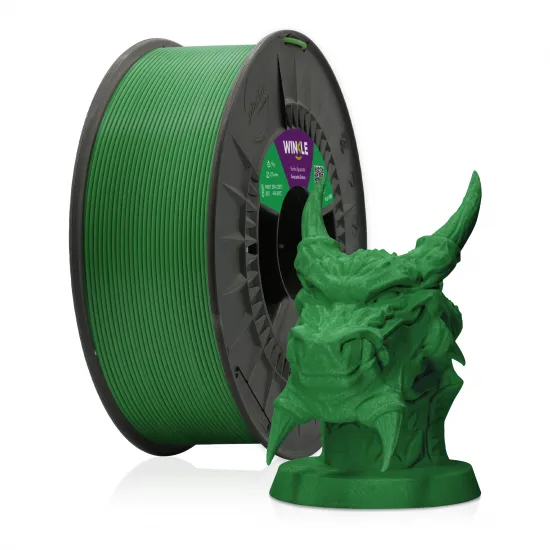
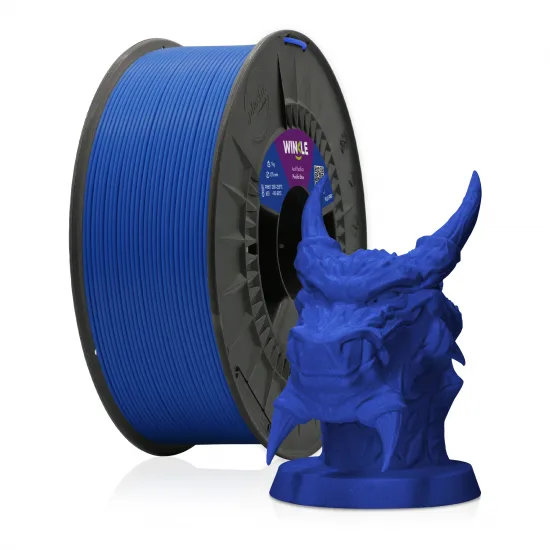
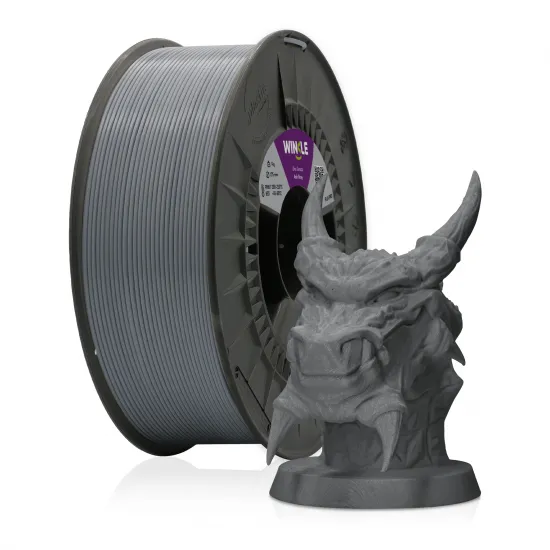
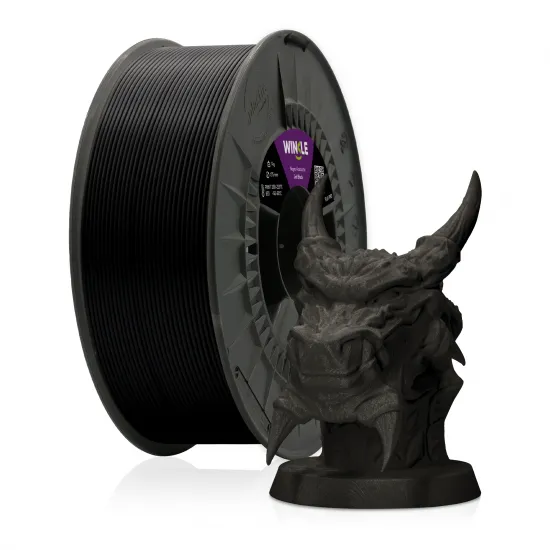
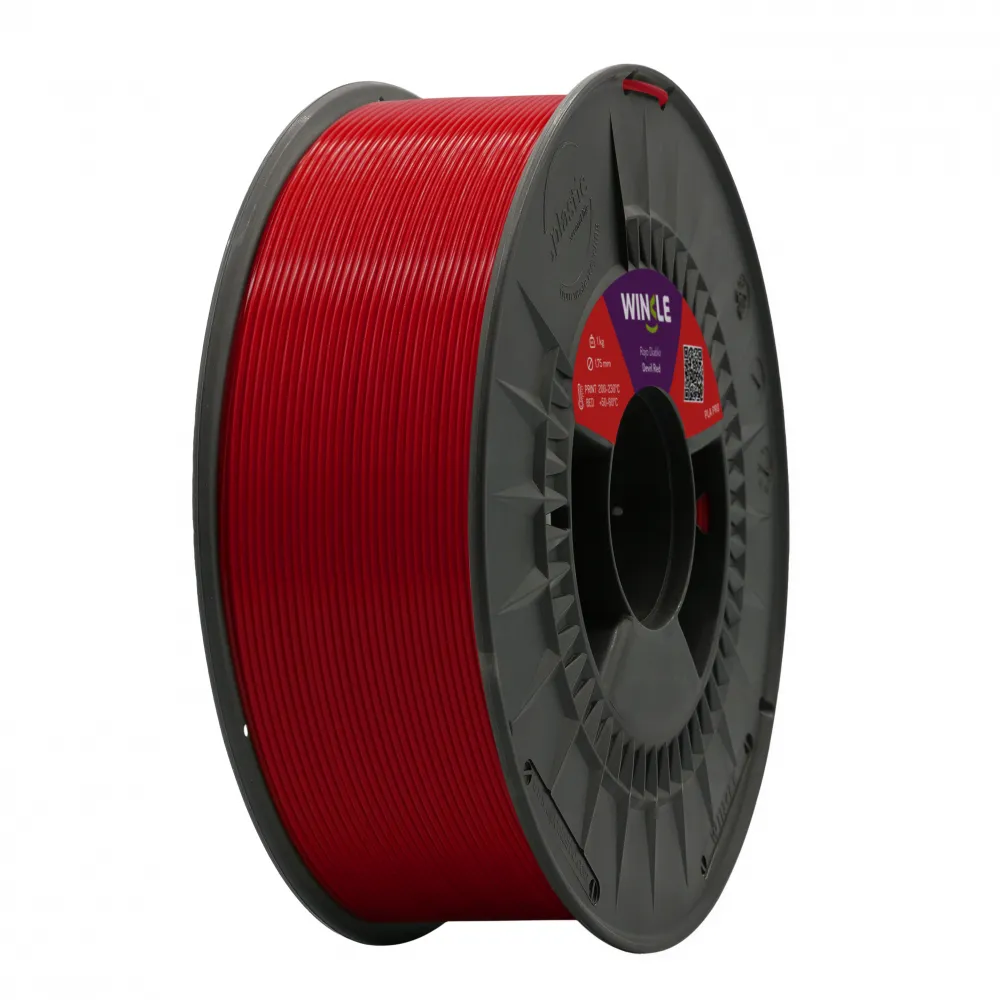
It is supplied as a 1 kg spool and is available in Glacier White, Canary Yellow, Devil Red, Avocado Green, Pacific Blue, Ash Gray and Jet Black, depending on current options. The photograph shows one variant; select the required colour before adding the product to your cart.
Declared technical properties
| Property | Nominal value | Reference |
|---|---|---|
| Specific gravity | 1.27 g/cc | ISO 1183 |
| Melting temperature | 205 ± 15 °C | Manufacturer data |
| Heat deflection temperature, HDT | 95 °C | ISO 75 |
| Tensile strength | 40 MPa | ISO 527 |
| Tensile modulus | 4000 MPa | ISO 527 |
| Charpy impact at 23 °C | 23 kJ/m² | ISO 179 |
These figures come from standardised material tests and do not automatically describe every printed part. Orientation, layer height, perimeter count, infill, interlayer bonding, geometry and annealing can substantially change final performance.
Recommended printing parameters
- Diameter: 1.75 mm.
- Net weight: 1 kg.
- Nozzle: 220-240 °C according to the official data sheet; 220-230 °C is a useful starting point for many printers.
- Bed: 50-60 °C.
- Recommended nozzle size: 0.4 mm.
- Initial speed: 50-80 mm/s.
- Cooling: up to 100% as a reference, reduced where stronger interlayer bonding is required.
- Chamber: open.
Start from a generic PLA profile near 225 °C and tune temperature, flow, retraction, cooling and pressure advance for your printer. WINKLE describes the material as capable of exceeding 120 mm/s, but this is not guaranteed on every machine: actual speed is limited by hotend volumetric flow, acceleration, cooling and part geometry. The published mass flow rate of 6 g/10 min at 210 °C/2.16 kg is a material test, not a maximum volumetric-flow value to enter directly into a slicer.
Annealing for improved thermal performance
The manufacturer associates the 95 °C HDT with correct annealing. Its reference process is around 110 °C: approximately 15-20 minutes for small parts and longer for large parts, potentially up to about 60 minutes. Place the part on a flat support, use temperature-controlled equipment and allow it to cool slowly before moving it.
Annealing may cause dimensional change or distortion. Test a coupon first, allow for critical dimensions and verify the finished part under its real operating conditions. A 95 °C HDT test figure does not guarantee 95 °C continuous service for every design.
3D-printer compatibility
It is suitable in principle for open-material FFF/FDM printers using 1.75 mm filament and capable of reaching the stated temperatures. With a properly tuned profile, examples include HTA3D HPRO, Prusa MK3/MK4, Creality Ender-3 and K1, Anycubic Kobra and Bambu Lab A1, A1 mini, P1 or X1. A shared filament diameter does not remove the need to check the material profile, feed path and spool dimensions.
WINKLE specifically declares compatibility with the Bambu Lab AMS Lite. For AMS, AMS 2 Pro or other automatic material systems, check spool support and filament path before assuming compatibility.
Choosing it against other PLA grades
- Choose PLA PRO when you want a balance of finish, mechanical strength and the option to improve thermal performance through annealing.
- For general use and maximum simplicity, see WINKLE PLA HD.
- If impact resistance is the priority, compare it with WINKLE PLA Tough.
- If maximum flow on a fast printer is the main goal, consider WINKLE PLA High Speed.
- If a specific raw-material flammability classification is required, review WINKLE PLA UL94 V0; PLA PRO must not be treated as equivalent.
Bed adhesion and storage
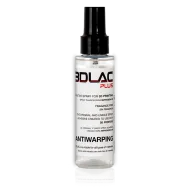
A clean build surface at 50-60 °C is normally sufficient. For difficult surfaces, large parts or surfaces requiring a release layer, use 3DLAC aerosol or 3DLAC Plus according to the adhesive instructions.
Store the spool sealed with desiccant and protected from moisture and heat. If you notice popping, bubbles, excessive stringing or an uneven surface, check drying condition before over-adjusting the profile.
It is for you if
You want a Spanish-brand PLA for prototypes and functional parts, value a semi-matte finish and need additional thermal headroom through a controlled annealing process.
It is not for you if
It is not the right choice if you need certified properties in the finished part, absolute dimensional stability after annealing, permanent high-temperature performance without validation or flame-retardant behaviour. Always test the actual geometry and process for critical components.