

- Stock: 1
- Model: PLA-UL94-V0-1.75mm

Type:

PLA HD

PLA HD Interference

PLA HD Sweet Pastel

PLA HD With particles

PLA HD GLOW

PLA HD SILK

PLA HD SILK Tricolor

PLA HD Transition

PLA HD Recycled

PLA Ingeo 3D850

PLA Ingeo 3D870

PLA Tough

PLA Matt

PLA High Speed

PLA PRO

PLA UL94 V0
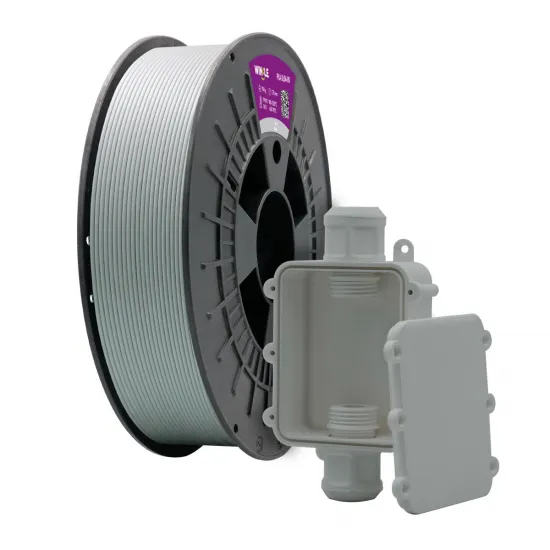
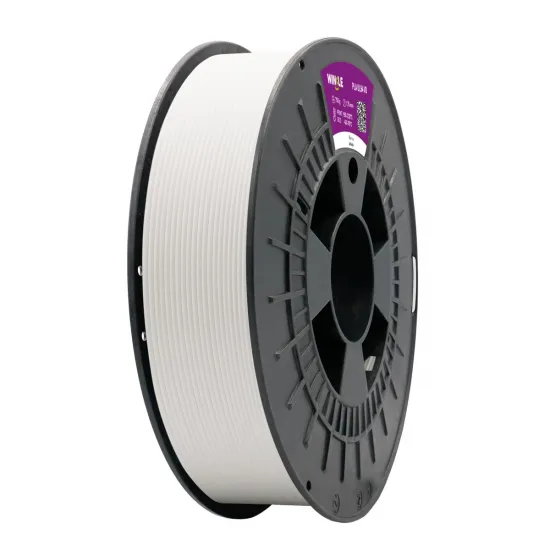
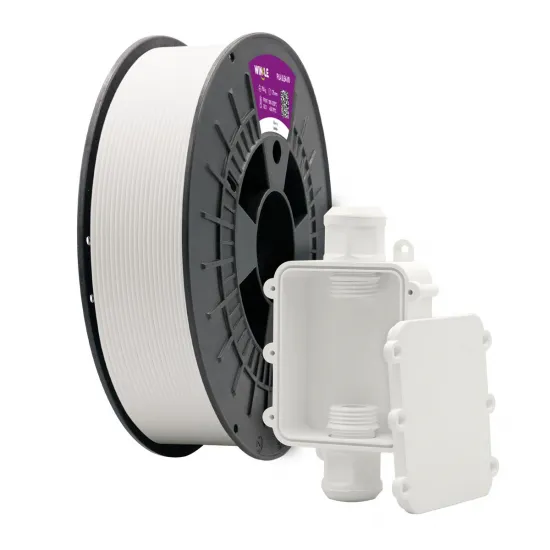
WINKLE PLA UL94 V-0 is a 1.75 mm white filament formulated to improve flame behaviour compared with conventional PLA. It retains relatively accessible printing, low warping and good stiffness, making it particularly useful for electronic enclosures, brackets, robotics, prototypes and auxiliary parts that will subsequently be validated for their final application.
WINKLE states that the raw material holds UL 94 V-0 certification and publishes a flammability test on five specimens with a V-0 result. This rating describes the behaviour of a small vertical specimen exposed to a controlled flame; it does not mean that the filament is non-combustible or automatically certify every printed part or finished device.
What UL 94 V-0 means
UL 94 V-0 is a flammability rating obtained through a small-scale vertical test. In the V-0 test, each flaming period after the burner is removed must end within 10 seconds; the set of applications must meet a total limit, burning must not reach the holding clamp and flaming drips must not ignite the cotton below the specimen.
The report published by WINKLE, dated 21 November 2023, rates the tested set as V-0: it states a 10-second maximum for an individual specimen, no flame or afterglow up to the clamp and no particles that ignite the cotton. The public documentation reviewed does not state the specimens' thickness, dimensions, orientation, print settings or colour, and does not include a UL file number.
A printed enclosure therefore does not automatically acquire V-0 certification. Where flame behaviour is a regulatory or safety requirement, the applicable documentation and exact material grade must be checked, and the finished part must be tested or certified using its actual thickness, geometry, colour, orientation, settings and production batch.
Format and key characteristics
| Material | PLA with flame-retardant additives; declared halogen-free formulation |
|---|---|
| Brand | WINKLE, Spanish manufacturer |
| Diameter | 1.75 mm |
| Net weight | 750 g |
| Colour | White |
| Nominal density | 1.31 g/cm³, ISO 1183 |
| Theoretical length | Approximately 238 m, calculated from weight, diameter and density |
| Packaging | Spool, reusable bag and silica desiccant |
The additives may produce visible particles in the filament and greater brittleness than standard PLA. WINKLE does not recommend it for high-load structural applications. Use smooth transitions, avoid excessively thin sections and test the part in its intended load orientation.
Nominal properties
The following figures come from the WINKLE technical data sheet and characterise the material under the stated methods. They are not guaranteed design values for every FFF part: orientation, perimeters, infill, layers, moisture, temperature and geometry can substantially change the result.
| Property | Nominal value | Stated method |
|---|---|---|
| Melt mass-flow rate, 210 °C / 5 kg | 10 g/10 min | ISO 1133 |
| Flexural modulus | 3,500–4,000 MPa | ISO 178 |
| Tensile modulus | 2,455 MPa | ISO 527 |
| Tensile yield strength | 60 MPa | ISO 527 |
| Tensile strength at break | 57 MPa | ISO 527 |
| Elongation at break | 2–4% | ASTM D638 |
| Charpy impact at 23 °C | 2.5–5 kJ/m² | ISO 179-1eA |
| Hardness | 80–85 Shore D | ASTM D2240 |
| Heat deflection temperature, HDT | 65 °C | ASTM D648; load not published |
| Melting temperature | Approximately 150–160 °C | Tm, DSC |
The 10 g/10 min figure is a material melt-flow rate measured under a 5 kg load; it is not 10 mm³/s and does not define a printer's maximum flow. The 65 °C HDT must not be treated as a universal continuous service temperature either.
Initial print profile
| Hotend temperature | 190–250 °C |
|---|---|
| Bed temperature | 50–60 °C |
| Speed | 40–60 mm/s |
| Part cooling | WINKLE publishes 100%; apply progressively after the first layers and tune for the part |
| Enclosure | Closed chamber recommended by WINKLE; actively heating the enclosure is not required |
| Nozzle | 0.4 mm or larger as a starting point |
The official 190–250 °C interval is broad. Start around the middle of the range, for example approximately 210 °C, and calibrate temperature, extrusion multiplier and flow for your hotend. Increase temperature only if layer bonding is insufficient or the extruder cannot maintain flow; reduce it if stringing, excessive gloss or soft detail appears.
Step-by-step tuning
- Check that the filament is dry, moves freely and the nozzle is clean.
- Start with the bed at 50–60 °C, a slow first layer and low or disabled cooling.
- Print a temperature tower within the official range and choose the section combining good finish and interlayer bonding.
- Calibrate flow and retraction at moderate speed before increasing acceleration or volumetric flow.
- Increase cooling after the first layers. If the part is weak between layers, reduce cooling or raise temperature slightly.
- When using an enclosed printer, avoid an excessively hot chamber: PLA can soften before the melt zone and cause heat creep.
Where build-plate adhesion is inconsistent, apply a thin film of 3DLAC aerosol bed adhesive or 3DLAC Plus concentrated adhesive, following the instructions for both the adhesive and build surface.
3D printer compatibility
It is conditionally compatible with 1.75 mm FDM/FFF printers capable of operating within 190–250 °C and maintaining a 50–60 °C bed. These conditions can be met by a correctly configured HPRO, Bambu Lab A1/P1/X1, Creality Ender-3/K1/CR-10, Prusa MK3/MK4/XL and Voron 2.4 or Trident, but each machine requires its own profile.
On enclosed machines, the enclosure helps prevent draughts, but unnecessary chamber heat should be avoided when printing PLA. Protect large parts from draughts on open machines. Compatibility with AMS, AMS Lite, AMS 2 Pro, MMU, CFS or other automatic material systems is not assumed: check spool dimensions, path and friction, or use an external spool holder.
Suitable applications
- Enclosures and covers for electronic prototypes.
- Mounts for boards, sensors, wiring and small equipment.
- Low-load robotics, automation and tooling parts.
- Prototypes intended to validate geometry and flame behaviour.
- Spacers, guides and auxiliary parts kept within the part's validated temperature range.
Safety and limitations
UL 94 is a flammability test, not a complete electrical-safety certification. On its own it does not establish electrical insulation, dielectric strength, arc resistance, comparative tracking index, continuous temperature rating, short-circuit resistance or suitability for mains or battery applications.
A printed part also does not replace fuses, protective earthing, insulation distances, thermal protection or an approved enclosure. Regulated equipment and critical applications require the relevant standards to be checked and the finished assembly to be tested. The material is not recommended for high-load structures or parts continuously exposed to temperatures close to its HDT.
Alternatives
If V-0 behaviour is not required and price, colours and general-purpose use take priority, WINKLE PLA HD 1.75 mm filament is a simpler option. If you need a PET-G-based flame-retardant formulation with a different balance of temperature, impact and chemical resistance, consider Sakata 3D PET-G V0 1.75 mm filament.
Storage
Keep the spool sealed with silica desiccant and protected from moisture, heat and direct sunlight. WINKLE does not publish a specific drying cycle for this grade; before applying heat, check that the spool and container can withstand it and follow the manufacturer's current instructions.
This is for you if
- You want a white PLA from a Spanish brand with declared V-0 behaviour.
- You need prototypes, supports or enclosures that can later be validated in their actual environment.
- You want a 750 g spool printable at normal PLA temperatures.
This is not for you if
- You need every printed part to be automatically UL certified.
- You need a non-combustible material or a substitute for the device's electrical and thermal safeguards.
- You require high ductility, a heavily loaded structural part or continuous high-temperature service.
Frequently asked questions
Will the filament always stop burning within 10 seconds?
That limit is part of the V-0 criterion for specific specimens and controlled conditions. It cannot be extended without testing to every part, thickness, orientation or real fire.
Is a printed enclosure automatically V-0 certified?
No. The available documentation does not identify the thickness and all settings of the tested specimens. If the rating is mandatory, the finished part or product must be validated and the required documentation checked.
Is 10 g/10 min the hotend's maximum flow?
No. It is the melt mass-flow rate measured to ISO 1133 at 210 °C under a 5 kg load. Actual print flow depends on the hotend, nozzle, temperature and required quality.
Does it need an enclosed printer?
WINKLE recommends a closed chamber. It can be printed on open machines when draughts and adhesion are controlled, while an enclosed printer should not be allowed to become excessively hot because this can promote PLA heat creep.
Package contents
- 1 × 750 g spool of 1.75 mm white WINKLE PLA UL94 V-0 filament in a reusable bag with silica desiccant.