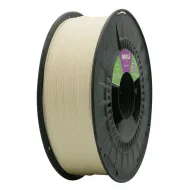
- Stock: 5
- Model: Easy-OFF-1.75mm-SAKATA3D

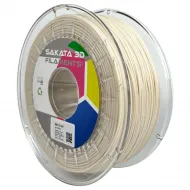
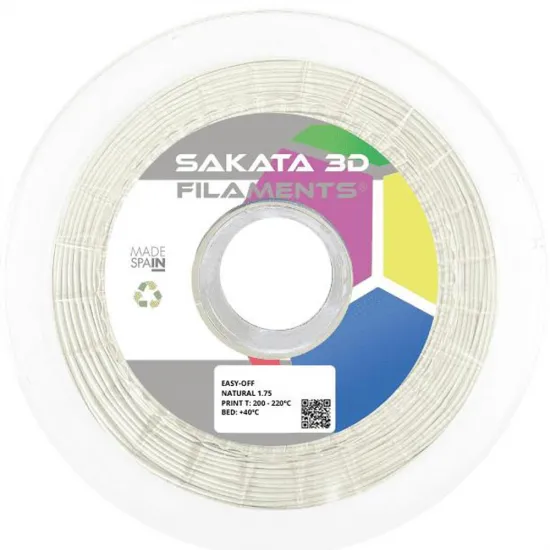
Sakata 3D PLA 450 Easy Off is a breakaway support filament for dual-material 3D printing. It is made from NatureWorks Ingeo 3D450 PLA and is designed to support overhangs, cavities and complex geometry during printing, while providing useful interface adhesion and easier mechanical removal afterwards.
This is not a soluble filament: supports are removed mechanically and do not require water or solvents. This simplifies post-processing and avoids the dissolution and storage requirements associated with PVA or BVOH, although the support interface still needs to be configured and calibrated correctly.
What is breakaway support used for?
When a model needs temporary material under an overhang or inside a cavity, printing the support from the same PLA requires an interface gap that can mark the surface. Easy Off allows a second material to be assigned to these areas and removed after printing. When correctly tuned, it can reduce support marks, make complex geometry easier to clean and shorten post-processing.
To use it automatically, the printer must handle two materials through two toolheads, dual nozzles, an IDEX system, a tool changer or a multi-material feeder. For many parts, using Easy Off only for the support-interface layers is an efficient way to reduce material use and tool changes.
Specifications
| Property | Value |
|---|---|
| Brand | Sakata 3D Filaments |
| Material | Support PLA based on NatureWorks Ingeo 3D450 |
| Removal method | Mechanical breakaway; not soluble |
| Nominal diameter | 1.75 mm |
| Net weight | 450 g |
| Colour | Natural |
| Nozzle temperature | 200-220 °C |
| Bed temperature | 40 °C or above as Sakata 3D's reference |
| Stated speed | Up to 100 mm/s with PLA 850 and PLA HR-870 under suitable conditions |
These values are starting points. Actual temperature must be tuned for the hotend, flow rate, residence time, model material and speed. The 100 mm/s limit does not guarantee the same result on every machine or geometry.
Material compatibility
Sakata 3D designed Easy Off to work with Ingeo 3D850 PLA 850 and Ingeo 3D870 HR-PLA. These are the combinations explicitly supported by the manufacturer's documentation.
Other PLA filaments sharing a suitable temperature window may be tested, but interface adhesion and release must first be verified with a sample. Compatibility with PETG, ABS, ASA, TPU, PA or PC must not be assumed: sharing the same diameter or temperature does not prove that two materials will form a stable interface while printing and separate safely afterwards.
Slicer setup
- Assign the model PLA to the main extruder and Easy Off to the support extruder or tool.
- To reduce consumption and changes, begin by using it only as the support interface.
- Use your slicer's standard interface values as a starting point, then tune layer count, density, Z gap and XY separation with a test print.
- On a single nozzle with material changing, configure a purge tower or the equivalent system. Insufficient purging can contaminate the interface; excessive purging increases time and waste.
- On dual-nozzle, IDEX or multi-tool systems, calibrate X/Y/Z offsets, relative nozzle height and ooze control before a long print.
- Check that active and standby temperatures do not degrade either material.
3D printer compatibility
It is a functional candidate for systems such as an Original Prusa XL with two or more toolheads, Original Prusa with MMU, Bambu Lab with AMS or AMS Lite, BCN3D IDEX printers and RepRap or Klipper machines with dual extruders or a tool changer. This list does not imply an official profile or automatic compatibility: verify 1.75 mm filament support, spool fit and feeding, the temperature window of both materials, purge strategy and slicer configuration.
A conventional single-material printer can change filament during a pause, but this is not a practical solution for supports distributed across many layers. If the machine cannot manage two materials, a dedicated breakaway support may offer little advantage over printing supports from the same PLA.
Support removal
- Allow the part to cool before handling it.
- Remove support progressively, starting with accessible areas.
- Use pliers and work gloves where sharp edges are present, as recommended by NatureWorks.
- Do not force thin walls, delicate details or enclosed cavities; divide the support into smaller sections if necessary.
- No water, limonene or other solvent is required.
Ingeo 3D450 reference properties
| Raw-material property | Method | Typical value |
|---|---|---|
| Specific gravity | ASTM D792 | 1.32 g/cm³ |
| MFR at 210 °C / 2.16 kg | ASTM D1238 | 18-26 g/10 min |
| Peak melt temperature | ASTM D3418 | 165-180 °C |
| Glass-transition temperature | ASTM D3418 | 55-60 °C |
NatureWorks identifies these as typical raw-material properties, not guaranteed specifications for the finished filament or a printed part. Easy Off is a temporary support material; it should not be selected as a structural material or its glass-transition temperature interpreted as a guaranteed service temperature.
Storage
Although Sakata 3D states that Easy Off is less moisture-sensitive than soluble support filaments, keep the spool sealed with desiccant. If popping, bubbles, stringing or inconsistent extrusion appear, use a conservative PLA-appropriate drying programme that is compatible with the spool. Industrial pellet-drying conditions must not automatically be copied as a consumer spool cycle.
This product is for you if
- You print PLA 850 or HR-870 and need mechanically removable supports or interfaces.
- Your printer and slicer can manage two 1.75 mm materials.
- You want to avoid solvents and reduce post-processing on complex geometry.
This product is not for you if
- You require soluble support for inaccessible cavities.
- Your printer only accepts one material and has no practical changing system.
- You need guaranteed compatibility with PETG, ABS, ASA, TPU or another material not declared by Sakata 3D.
Printing in an area with suitable general ventilation is recommended. Ingeo 3D450 is not certified for food-contact or medical applications.