

- Stock: 3
- Model: 60A-Filaflex-PRO

Model:

95A Medium-Flex

82A FIlaflex

70A Filaflex UltraSoft

Filaflex 60A PRO
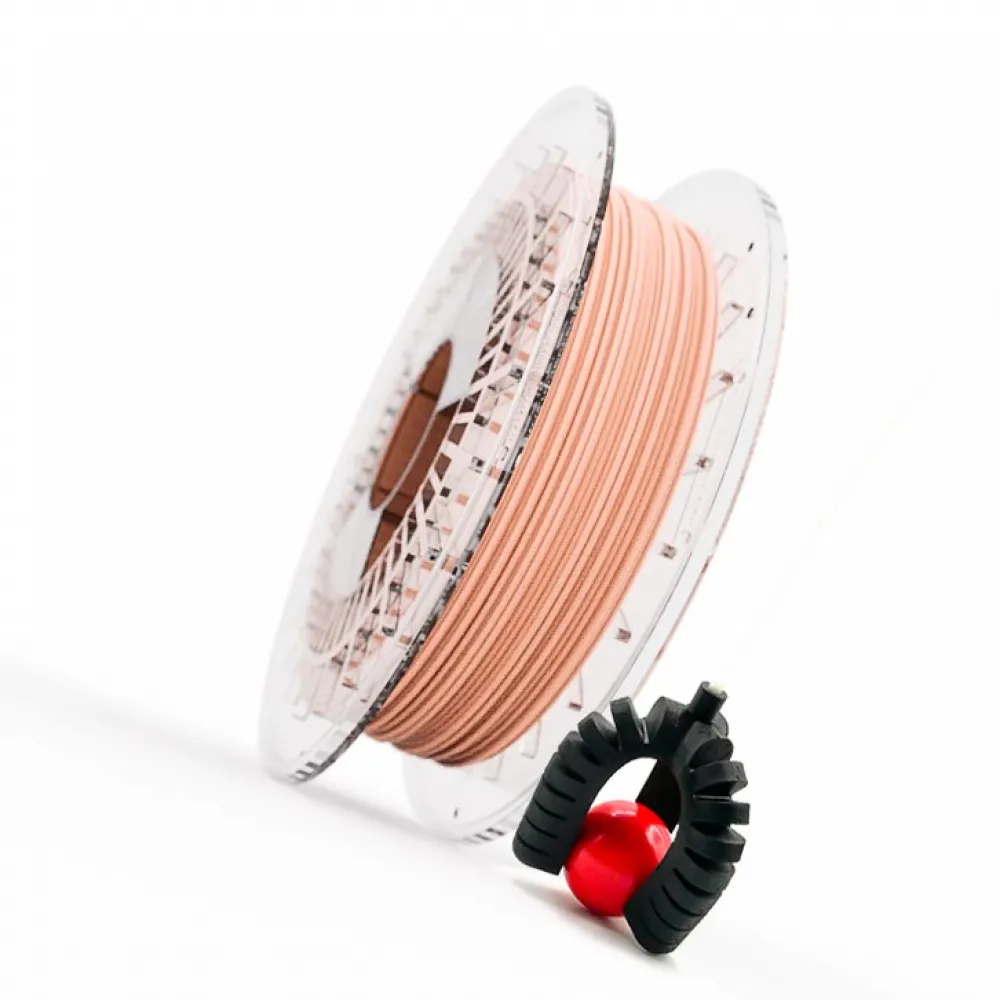
Recreus Filaflex 60A PRO is a Spanish-made 1.75 mm TPU filament for printing exceptionally soft, elastic parts with reliable shape recovery. It is the most flexible grade in the Filaflex range and is intended for experienced users with direct drive and an especially well-constrained filament path.
Its nominal 60 Shore A hardness and elongation at break of up to 950% enable seals, buffers, grippers, insoles, soles, textiles and ergonomic prototypes with deformation that conventional 95A TPU cannot readily provide. That advantage also makes it much more demanding to print: this is not the recommended grade for a first flexible-filament project.
Material technical properties
Recreus markets this grade as 60A, while its technical data sheet measures 63 Shore A after 3 seconds according to ISO 7619-1. This reflects the difference between a nominal grade and the result of a specific test.
| Property | Value | Method |
|---|---|---|
| Material | TPU, flexible thermoplastic polyurethane | Recreus |
| Density | 1.07 g/cm³ | ISO 1183 |
| Tested hardness | 63 Shore A, 3 s reading | ISO 7619-1 |
| Tensile strength | 26 MPa | DIN 53504-S2 |
| Elongation at break | 950% | DIN 53504-S2 |
| Stress at 20 / 100 / 300% | 1 / 2.5 / 4.5 MPa | DIN 53504-S2 |
| Tear strength | 40 N/mm | ISO 34-1 |
| Abrasion loss | 45 mm³ | ISO 4649 |
| Glass transition | -54 °C | ISO 11357-1/-2 |
| Vicat softening | 70 °C, method A | ISO 306 |
| HTA3D format | 1.75 mm - 500 g | Product supplied |
These figures refer to the material or standard specimens. A printed part may vary with moisture, orientation, temperature, layer bonding, geometry, wall thickness, perimeters and infill. The Vicat value is not, by itself, a maximum service temperature.
Available colours
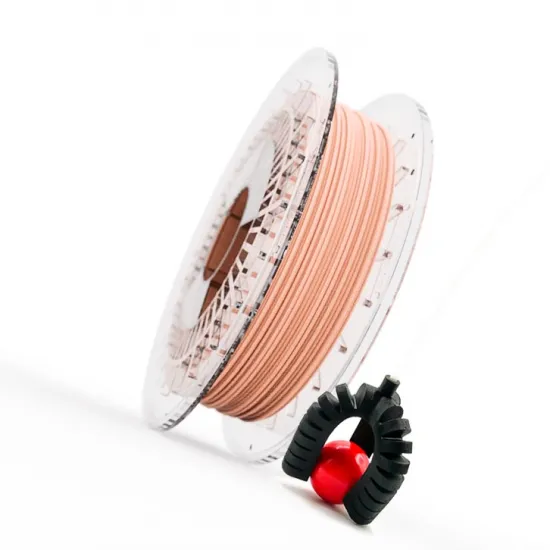
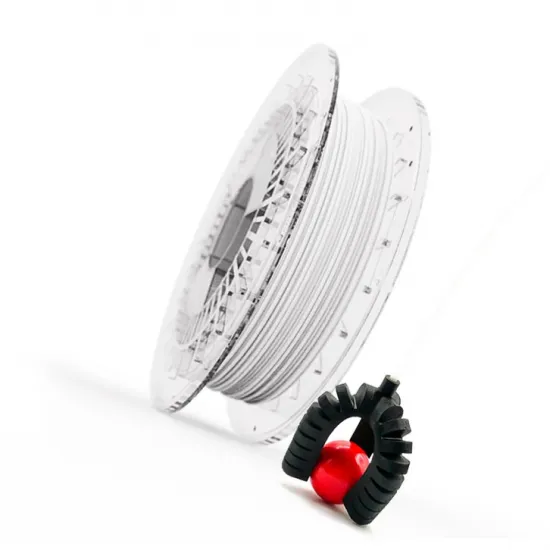
This product is available in white and nude or skin tone, both as 1.75 mm filament on a 500 g spool. Availability may vary; select the required colour before adding the product to the cart.
Current Recreus starting parameters
The current official documentation uses 235 °C and limits volumetric flow by nozzle size. These figures replace older, cooler recommendations. They are starting points that must be tuned on the actual printer.
| Nozzle | Layer | Line width | Initial flow | Temperature |
|---|---|---|---|---|
| 0.4 mm | 0.20 mm | 0.34 mm | 2.0 mm³/s | 235 °C |
| 0.6 mm | 0.30 mm | 0.54 mm | 4.5 mm³/s | 235 °C |
| 0.8 mm | 0.40 mm | 0.74 mm | 8.0 mm³/s | 235 °C |
| 1.0 mm | 0.50 mm | 0.94 mm | 12.5 mm³/s | 235 °C |
Filaflex 60A can stretch during extrusion and produce a line slightly narrower than the nozzle. Retain the associated line width and layer height when transferring the flow limit to your slicer.
Reference linear speeds
| Nozzle | External | Internal | Infill | Top/bottom | First layer |
|---|---|---|---|---|---|
| 0.4 mm | 15.15 mm/s | 22.73 mm/s | 30.30 mm/s | 18.18 mm/s | 9.09 mm/s |
| 0.6 mm | 14.15 mm/s | 21.23 mm/s | 28.30 mm/s | 16.98 mm/s | 8.49 mm/s |
| 0.8 mm | 13.70 mm/s | 20.55 mm/s | 27.40 mm/s | 16.44 mm/s | 8.22 mm/s |
| 1.0 mm | 13.44 mm/s | 20.16 mm/s | 26.88 mm/s | 16.13 mm/s | 8.06 mm/s |
Retraction
| Nozzle | Starting distance | Speed | Z-hop |
|---|---|---|---|
| 0.4 mm | 1.5-2.0 mm | 30 mm/s | 0.2 mm |
| 0.6 mm | 1.5-2.5 mm | 30 mm/s | 0.2 mm |
| 0.8-1.0 mm | 2.0-3.5 mm | 30 mm/s | 0.2 mm |
Reduce retraction if the filament compresses or stops feeding. To reduce stringing, use the highest travel speed that your machine can perform safely and reliably; do not copy 200-500 mm/s if the mechanics are not designed for it.
Bed, cooling and drying
- Drying: 55 °C for at least 1 hour before printing.
- Small parts: bed at room temperature.
- Large parts: start at 40-45 °C.
- Cooling: 0% in general and on the first layer; up to 40% only for layers shorter than 10 seconds if required.
- Adhesive: normally unnecessary. If a particular surface or geometry has poor adhesion, tune the first layer first and only add an adhesion aid when needed.
Extruder, hotend and filament path
This grade works best with direct drive. The path between the drive gears and hot zone should be short, continuous and fully constrained: a small gap can allow the TPU to compress, buckle or escape sideways.
- Start with moderate idler pressure; excessive force flattens the filament.
- Avoid tight bends and friction between the spool and extruder.
- Check that the nozzle is clean before loading.
- Reduce flow, acceleration or retraction if feeding becomes inconsistent.
- Bowden: Recreus does not recommend it for Filaflex 60A.
Compatibility with specific printers
Recreus publishes starting profiles for Bambu Lab P1P/P1S, X1/X1C/X1E, A1/A1 mini, P2S, H2S and H2D, plus Original Prusa MK4/MK4S, CORE One/CORE One+/CORE One L and Prusa XL. The profile supports those families, but machine revision, nozzle, feeding path and current instructions must still be checked before printing.
A Bambu or Prusa profile does not mean that the filament can travel through an AMS, AMS Lite, MMU or another automatic feeder. With 60A TPU, direct feeding from an external spool is preferable unless the system explicitly supports that hardness.
Other direct-drive printers may be compatible when the path is fully constrained and a conservative profile is carefully tuned. Compatibility is not automatic: two direct-drive toolheads can behave very differently.
Controlling finished-part flexibility
Shore hardness describes the material but does not determine finished feel by itself. A thin wall with few perimeters and low infill will be highly deformable; increasing wall thickness, perimeters or infill raises compression resistance. Print specimens using the actual geometry before finalising a functional design.
Skin contact and regulated applications
Recreus holds ISO 10993 cytotoxicity, irritation and sensitisation test reports for an identified Filaflex sample, together with a declaration that includes white and nude Filaflex 60A. These documents support the tested material but do not automatically certify a finished printed part.
Food-contact, medical, orthopaedic or prolonged skin-contact applications require validation of the batch and colour, printing process, additives, cleaning, geometry and actual use conditions. A medical device or commercial article requires the applicable risk assessment and finished-product testing. This material is not intended for implants.
Applications
- Exceptionally soft seals, buffers, dampers and protectors.
- Grippers, wheels, tyres and soft-robotics components.
- Insoles, soles, footwear and ergonomic prototypes.
- Textiles, accessories and parts that must stretch and recover.
- Anatomical models and non-implantable prototypes, subject to appropriate validation.
Resistance to fuels or solvents depends on substance, concentration, temperature, time and load. Test the finished part before any critical use.
Troubleshooting
- Bubbles, popping or rough surface: dry the filament and test again.
- Irregular extrusion: inspect the nozzle, path and idler; then reduce flow and speed.
- Stringing: dry first, then tune retraction, temperature and travel.
- Small layers deform: print several parts together or allow more cooling time between layers.
- First layer bonds too strongly: reduce squish; adhesive is normally unnecessary.
Choosing within the Filaflex range
- Filaflex 95A Medium-Flex: the firmest, fastest and easiest grade to feed.
- Filaflex 82A Original: high flexibility with intermediate difficulty.
- Filaflex 70A Ultra-Soft: very soft and demanding, but somewhat easier than 60A.
- Filaflex 60A PRO: maximum deformation and softness for specially prepared setups.
It is for you if
- You need a substantially softer and more elastic part than 95A, 82A or 70A TPU.
- Your printer has direct drive and a short, fully constrained path.
- You can dry the spool and spend time tuning flow, retraction and part design.
It is not for you if
- You are choosing your first flexible filament or prioritise speed and ease of printing.
- Your printer uses a long Bowden tube or has gaps in the filament path.
- You need to feed it through an automatic system that does not confirm support for 60A TPU.
- You need a medical, food-contact or safety-critical part ready for use without additional validation.