

- Stock: 15
- Model: Nozzle-coated-0.4

Model:

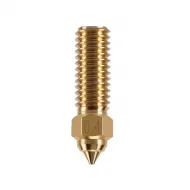
Brass 0.20 to 1.00mm

Teflon coated 0.3mm

Teflon coated 0.4mm

Stainless steel 0.4mm

Stainless steel 0.6mm
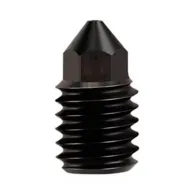
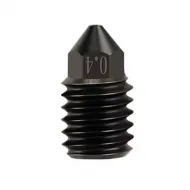
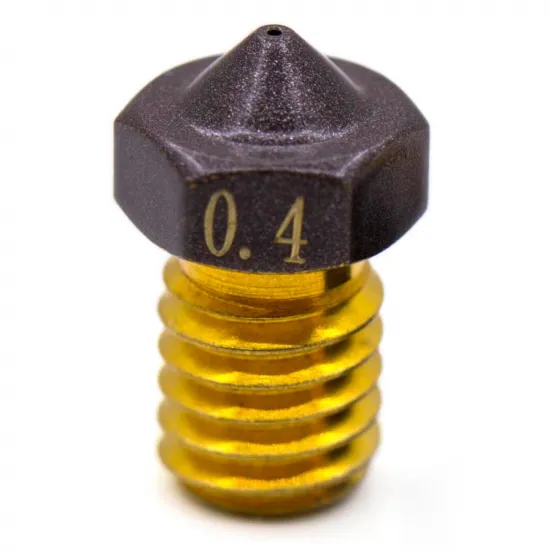
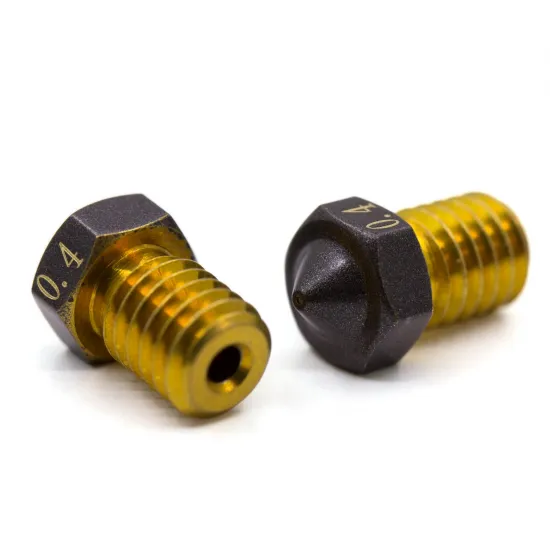
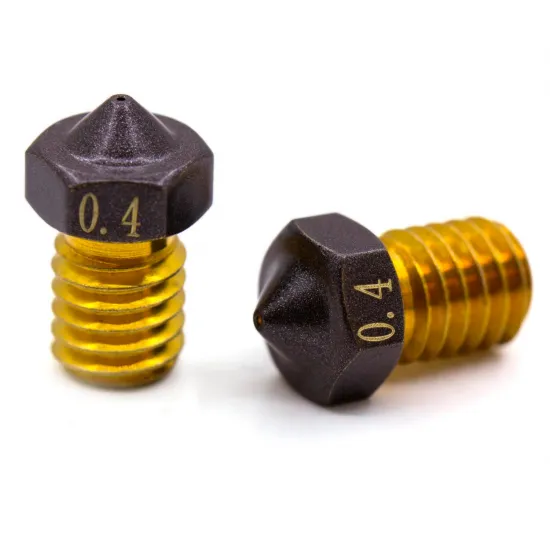
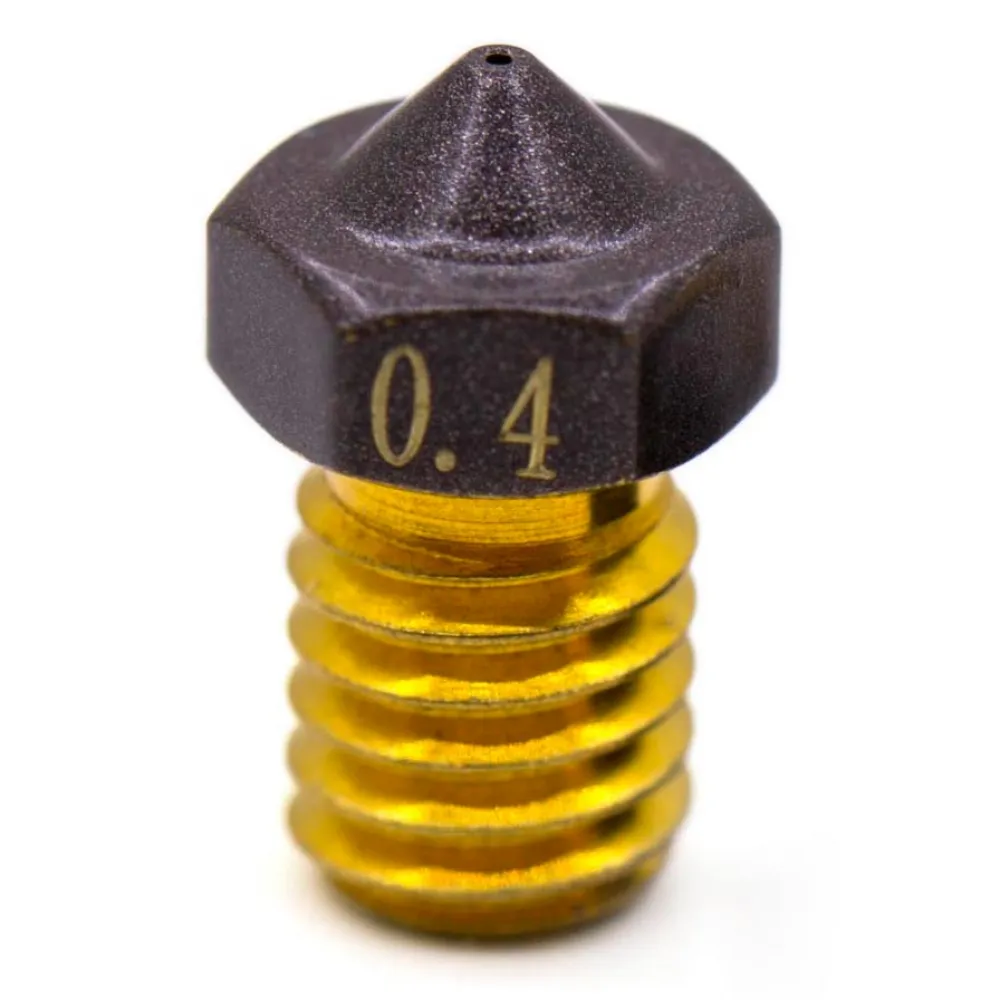
V6-style brass nozzle for 1.75 mm filament, with a nominal 0.4 mm outlet and an external non-stick coating. It is a general-purpose size balancing detail, line strength, ease of tuning and print time.
The dark finish covers the outer cone and hex to help reduce plastic buildup and simplify cleaning. The core remains brass: it retains good heat transfer, but does not become abrasion resistant.
Technical specifications
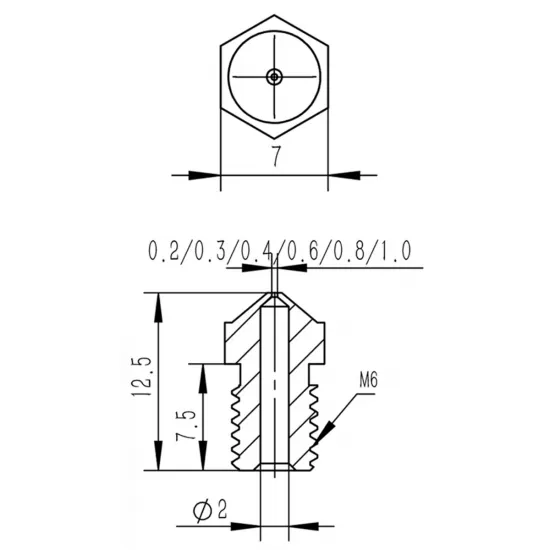
| Material | Brass with external non-stick coating |
|---|---|
| Filament | 1.75 mm |
| Nominal outlet | 0.4 mm |
| Thread | M6 |
| Overall / threaded length | 12.5 mm / 7.5 mm |
| Hex | 7 mm spanner |
| Nominal rear inlet | Ø2 mm |
| Package contents | 1 nozzle |
Compatibility: check the complete geometry
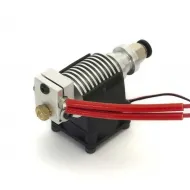
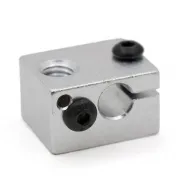
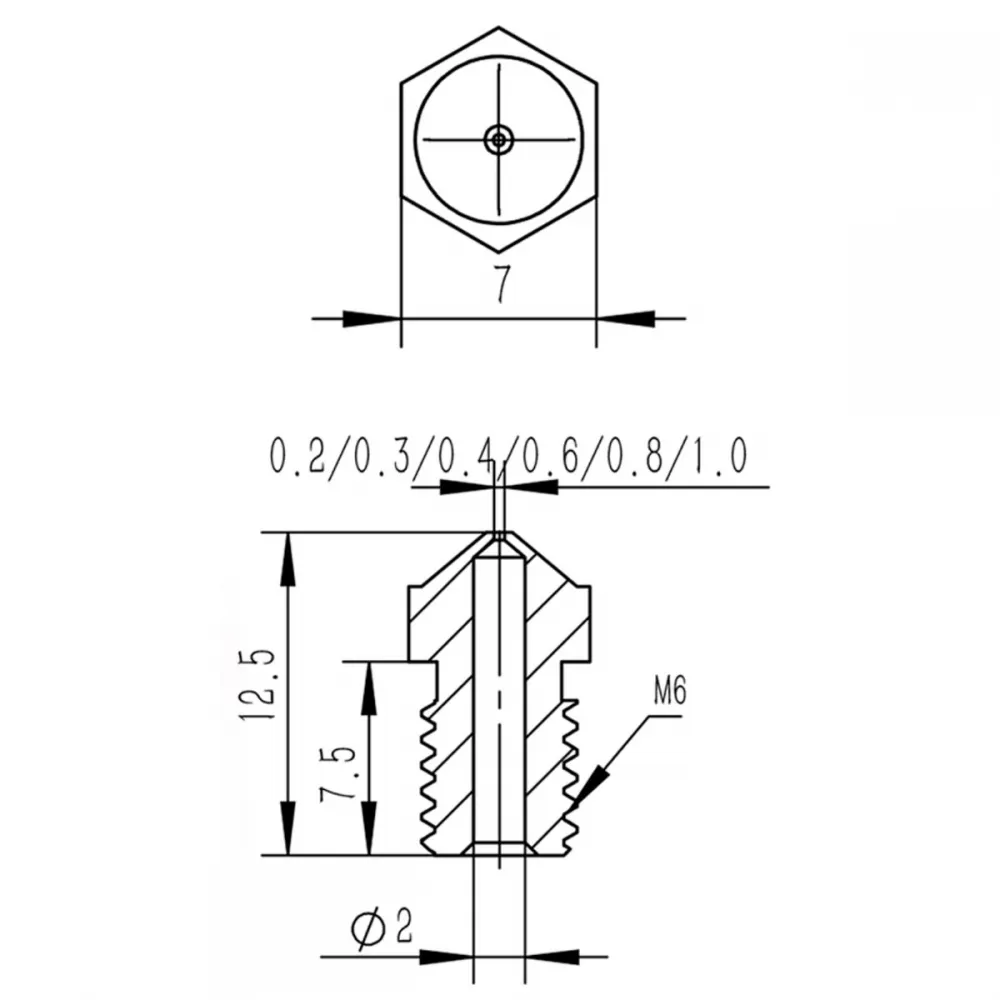
It is dimensionally compatible with blocks and hotends that use a short V6-style nozzle for 1.75 mm filament, with an M6 thread, 12.5 mm overall length, 7.5 mm threaded section, 7 mm hex and sealing against the heatbreak. It can, for example, be combined with our V6 aluminium heater block or V6 brass heater block for 3 mm sensors, after checking the rest of the assembly.
An M6 thread alone does not guarantee compatibility. It is not a direct substitute for Revo, Volcano, SuperVolcano, different-length MK8, Creality K1 or integrated cartridge nozzles. On Prusa, Voron and other modified machines, identify the hotend actually installed.
Use and materials
The 0.4 mm outlet suits most common PLA, PETG, ABS, ASA or TPU profiles within the hotend limits. It supports familiar layer heights and line widths while retaining a reasonable level of detail.
Brass is not abrasion resistant. Carbon- or glass-fibre fillers, mineral or metal particles, wood, glow filaments and some pigments can wear and enlarge the outlet despite the external coating. Use a purpose-made wear-resistant nozzle for these materials.
For particularly fine details, see the 0.3 mm version in the same format.
Installation, sealing and maintenance
- Unload the filament and provide safe access without straining heater or sensor wires.
- Hold the heater block with a suitable tool and use a 7 mm spanner on the nozzle; do not transfer force through the heatbreak.
- Thread it in without cross-threading. The nozzle must seal against the heatbreak inside the block and leave a small visible gap between the hex and block.
- Perform final hot tightening using the hotend manufacturer's procedure and torque. For its own brass V6 assembly, E3D specifies 285 °C and 2 N·m; do not transfer these values if any part in your assembly has a lower limit.
- After replacement, check the joint for plastic leakage and recalibrate the first layer.
Clean the exterior using a non-abrasive method. Blades, steel brushes, abrasives or flame may damage the finish. The coating helps with external residue but does not prevent internal clogs.
Slicer and firmware
| System | Adjustment |
|---|---|
| Slicer | Select 0.4 mm and review line width, layer height, speed and volumetric flow. Start with a conservative profile. |
| Marlin | Nozzle diameter is normally handled in the slicer; replacing the nozzle alone does not require recompilation. |
| Klipper | Set nozzle_diameter: 0.4 in [extruder] and use the same value in the slicer. |
| RepRapFirmware | The diameter is normally defined in the slicer; review any custom macros or limits that depend on it. |
Check Z offset after installation. PID autotuning is usually only needed if maintenance has noticeably changed thermal response. No independent maximum temperature is declared for this coating: always respect the lowest limit in the complete hotend and choose a nozzle with traceable specifications for high-temperature use.