

- Stock: 154
- Model: Nozzle-1.75 Inox-0.4
Model:

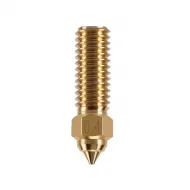
Brass 0.20 to 1.00mm

Teflon coated 0.3mm

Teflon coated 0.4mm

Stainless steel 0.4mm

Stainless steel 0.6mm
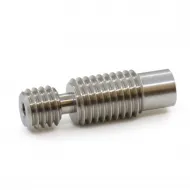
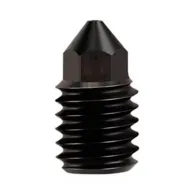
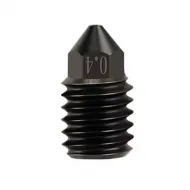
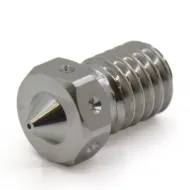
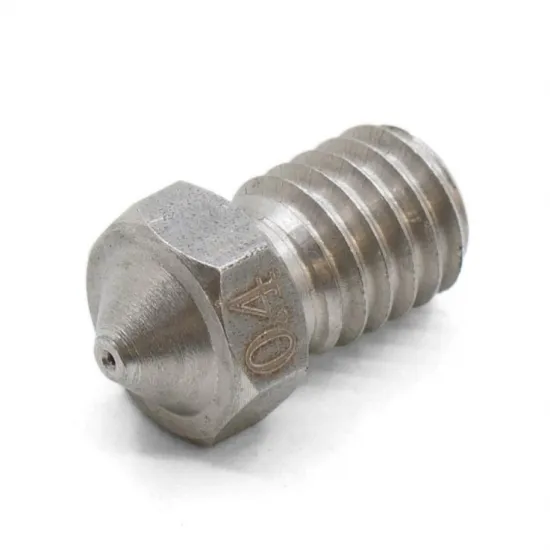
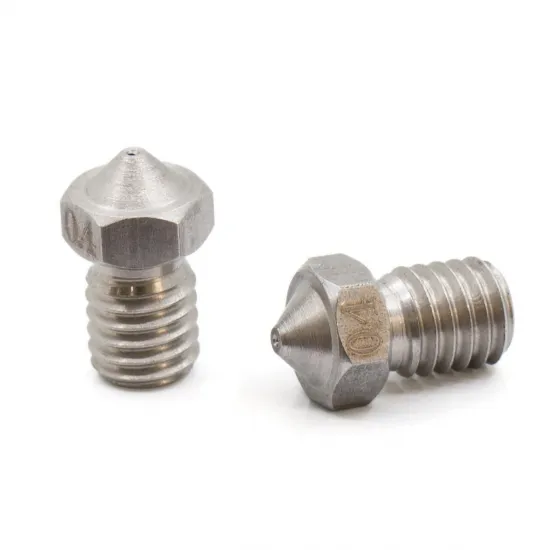
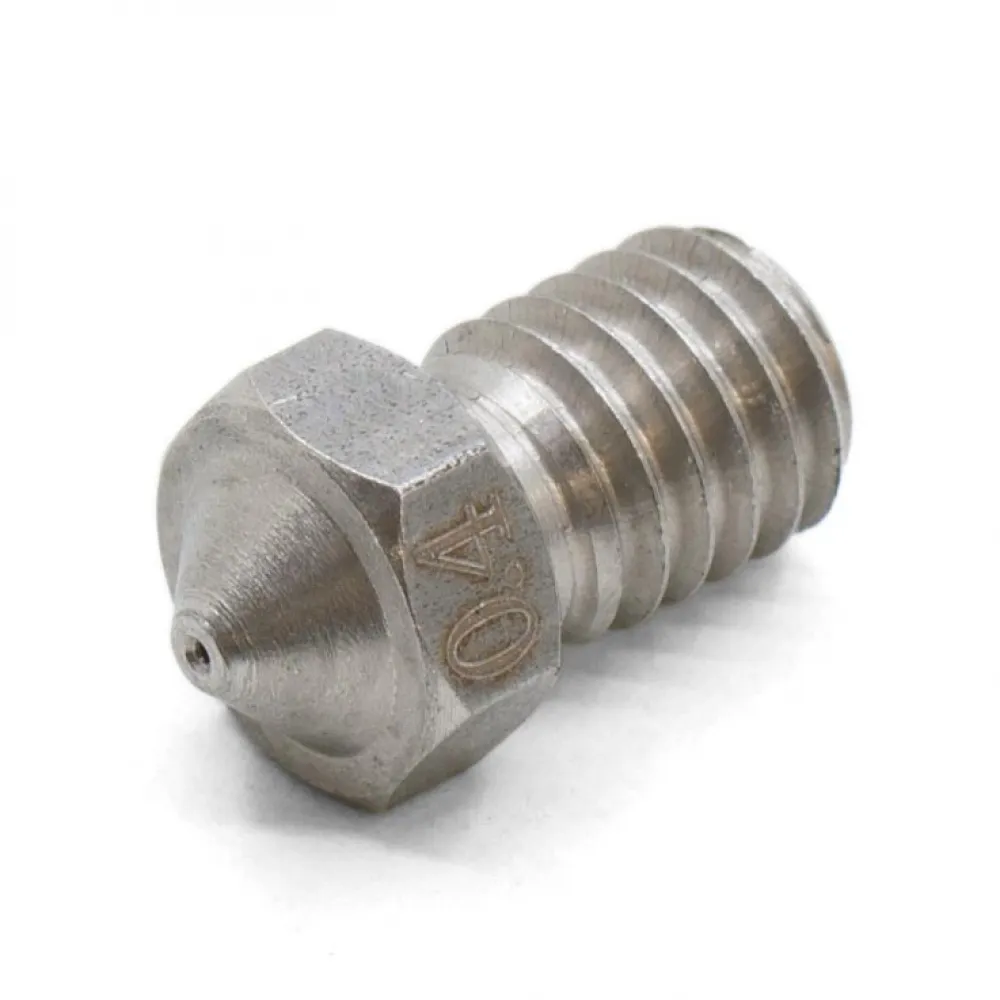
Stainless-steel nozzle for 1.75 mm filament, with a nominal 0.4 mm outlet and short V6-style geometry. This is a versatile size for common print profiles and an alternative to brass where stainless steel is preferred.
Technical specifications
| Material | Stainless steel |
|---|---|
| Filament | 1.75 mm |
| Nominal outlet | 0.4 mm |
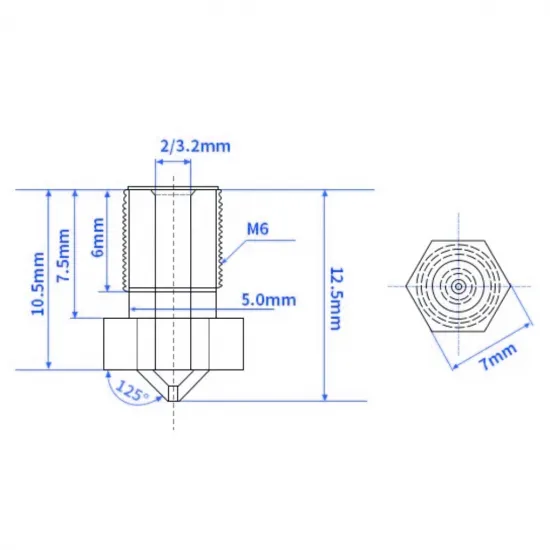
| Thread | M6 |
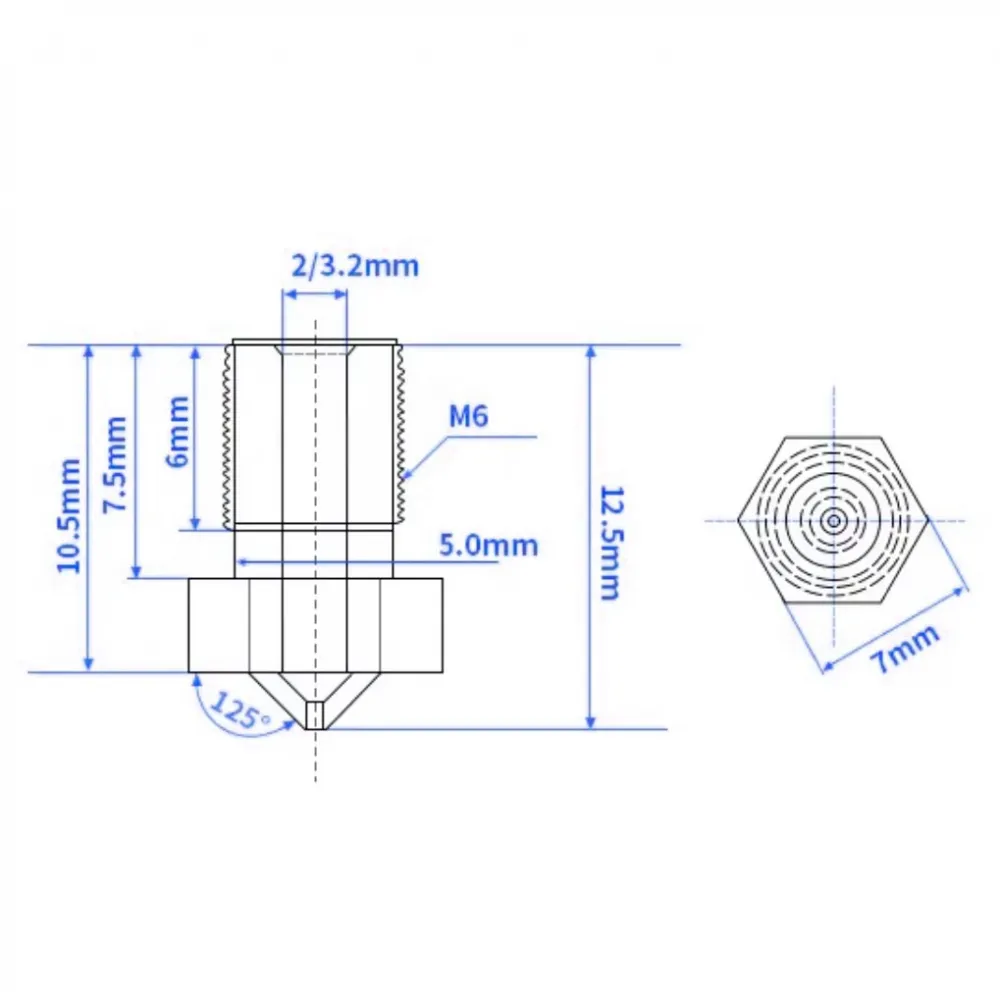
| Overall length | 12.5 mm |
| Nominal threaded section | 6 mm |
| Hex | 7 mm spanner |
| Nominal rear inlet | Ø2 mm |
| Package contents | 1 nozzle |
Compatibility
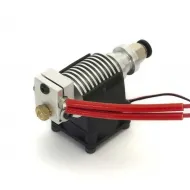
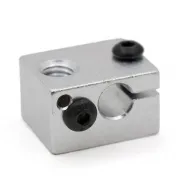
It is dimensionally compatible with blocks and hotends using a short V6-style nozzle for 1.75 mm filament, with an M6 thread, 12.5 mm overall length, 7 mm hex and sealing against the heatbreak. It can be paired with our V6 aluminium heater block or V6 brass heater block for 3 mm sensors, after checking the rest of the assembly.
An M6 thread alone does not guarantee compatibility. It is not a direct substitute for Revo, Volcano, SuperVolcano, different-length MK8, Creality K1 or integrated cartridge nozzles. On Prusa, Voron and modified machines, check the hotend actually installed.
Stainless steel and abrasive materials
Stainless steel does not mean hardened steel. This nozzle is not advertised as abrasion resistant. Carbon- or glass-fibre fillers, metal or mineral particles, wood, glow additives and some pigments may wear its outlet.
Use a hardened or specifically wear-rated nozzle for abrasive materials. It should not automatically be considered suitable for food or medical applications either: the alloy, cleaning, filament, machine and complete process would require specific validation.
Installation and settings
- Unload the filament and access the heater block without straining heater or sensor wires.
- Hold the block and use a 7 mm spanner. The nozzle must seal against the heatbreak rather than the outside face of the block.
- Perform final hot tightening according to the hotend manufacturer's procedure and limits. For its own stainless V6 nozzle, E3D specifies heating 20 °C above printing temperature and applying 2 N·m; use these values only if the complete assembly permits them.
- Check for leaks and recalibrate the first layer and Z offset.
Select 0.4 mm in the slicer. In Klipper use nozzle_diameter: 0.4; Marlin and RepRapFirmware normally obtain nozzle size from the slicer workflow. As stainless steel transfers heat differently from brass, check temperature, speed and flow with a test rather than applying a fixed temperature increase.
For wider lines or higher flow, see the 0.6 mm stainless-steel version.