

- Stock: 4
- Model: Reciflex-Recreus

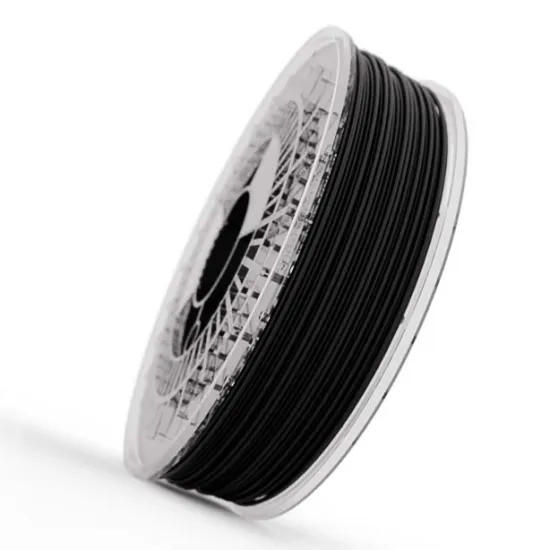
Recreus Reciflex recycled 96A-98A black TPU 1.75 mm — 750 g
Recreus Reciflex is a flexible TPU filament made in Spain from 100% recycled sources. It combines selected waste from the local footwear industry with material recovered from Recreus production processes, reducing waste while providing a feedstock prepared specifically for FDM/FFF 3D printing.
Its stated hardness ranges from 96A to 98A Shore. This is a relatively firm flexible material: it retains deformation and recovery while generally being easier to feed than softer 82A or 85A grades. The material is selected and magnetically screened during production, then pigmented black to homogenise feedstock originating from different colours.
Main features
| Manufacturer | Recreus, Spain |
|---|---|
| Material | TPU from 100% recycled sources |
| Diameter | 1.75 mm |
| Net weight | 750 g |
| Current stated hardness | 96A-98A Shore |
| Colour | Black |
| Reference density | 1.00-1.22 g/cm³, ISO 1183 |
| Reference elongation at break | Over 400%, internal Recreus test |
| Reference tensile strength | 40-50 MPa, internal Recreus test |
The ranges reflect the natural variability of recovered feedstock. They are reference technical data rather than guaranteed tolerances for every printed part, as orientation, infill, moisture, temperature and processing also affect the result.
Recommended printing parameters
The current official guide uses different temperatures and volumetric limits for each nozzle. Treat them as starting points and verify the actual flow capability of your hotend:
| Nozzle | Layer height | Line width | Initial flow limit | Temperature |
|---|---|---|---|---|
| 0.4 mm | 0.2 mm | 0.40 mm | 4.5 mm³/s | 245 °C |
| 0.6 mm | 0.3 mm | 0.60 mm | 10.1 mm³/s | 245 °C |
| 0.8 mm | 0.4 mm | 0.80 mm | 18.0 mm³/s | 248 °C |
| 1.0 mm | 0.5 mm | 1.00 mm | 28.1 mm³/s | 250 °C |
As a reference, Recreus proposes approximately 28 mm/s for external perimeters, 42 mm/s for internal perimeters, 56 mm/s for infill, 34 mm/s for top and bottom surfaces and 17 mm/s for the first layer. Reduce flow if the extruder compresses the filament, the hotend loses temperature or extrusion becomes irregular.
Drying, bed and cooling
- Drying: 55 °C for at least 1 hour before printing.
- Small parts: unheated bed at room temperature.
- Large parts: bed at 50-55 °C.
- Part cooling: normally 0%; also 0% on the first layer.
- Very short layers: up to 40% cooling when a layer takes less than 20 seconds.
Keep the spool sealed and dry, preferably with desiccant. The safety data sheet specifies storage below 40 °C. If you notice bubbles, a rough surface, popping or difficult stringing, dry the filament before changing several print settings at once.
Extruder and retraction
Recreus preferably recommends a direct-drive extruder and reduced idler pressure to avoid crushing the TPU. The filament path should remain closely constrained from the drive gears to the hotend, without gaps where it can buckle. The HTA3D direct extruder optimised for flexible filament is an option for machines mechanically compatible with its geometry.
| Nozzle | Initial retraction | Speed | Z-hop |
|---|---|---|---|
| 0.4-0.6 mm | 1.8-2.5 mm | 40 mm/s | 0.2 mm |
| 0.8-1.0 mm | 2.0-3.0 mm | 40 mm/s | 0.2 mm |
These are manufacturer starting points. On a direct-drive system, reducing distance may help if retraction deforms the filament or causes irregular feeding. Fast travel can reduce stringing, but it must remain within the printer's verified mechanical limits.
3D printer compatibility
No flexible filament is automatically compatible with every printer. The machine must accept 1.75 mm filament, reach the stated temperature and have an extruder capable of guiding TPU without buckling.
Recreus currently provides profiles for Bambu Lab A1 and A1 mini, P1P and P1S, X1, X1C and X1E, P2S, H2S and H2D, plus Prusa MK4/MK4S, CORE One, CORE One+ and CORE One L, and Prusa XL. Profile availability provides a useful starting route but does not replace checks for hotend, machine revision or filament path.
- Bambu Lab: use an external spool unless Bambu explicitly documents this exact material and machine combination for its AMS or automatic feeding system.
- Prusa and HPRO direct-drive machines: the short filament path is favourable; tune flow, retraction and idler pressure for the actual unit.
- Ender-3, CR-10 and other Bowden machines: may need a short, closely constrained Bowden path, lower speeds or a direct-drive conversion. Operation with the original extruder is not guaranteed.
Applications
- Cases, bumpers, protectors and impact-absorbing parts.
- Drone bumpers and guards.
- Wheels, tyres and flexible components for robotics or radio-control models.
- Gaskets, supports, grips and deformable components.
- Prototypes and end-use parts where recycled origin is a relevant requirement.
The solvent resistance stated by Recreus is a general material property. For contact with a specific chemical, print and test a representative coupon under the intended concentration, temperature, exposure time and mechanical load. This product is not presented as certified for food, medical or safety-critical use.
Comparison with other flexible filaments
- Recreus Filaflex 95A offers similar hardness with feedstock not declared as recycled.
- Recreus Filaflex 82A creates substantially softer parts but also requires more carefully controlled feeding.
- Sakata 3D recycled RE-FLEX 85A is a softer recycled alternative when greater deformation is required.
It is for you if
- You want a relatively firm flexible TPU made from recycled-origin material.
- You need black impact-resistant parts that can deform and recover.
- Your printer has a closely guided filament path and configurable print settings.
It is not for you if
- You require an exact fixed hardness outside the stated 96A-98A range.
- You need a biodegradable material: recycled and biodegradable are not equivalent.
- You require certified chemical resistance, food contact or a specific medical approval.
- Your extruder has open gaps where TPU can buckle and the feed path cannot be modified.
Safety
Print with sufficient ventilation and avoid breathing vapours or decomposition products. Molten polymer can adhere to skin and cause burns. Keep the material away from flames and ignition sources and do not inhale smoke in the event of combustion.
Package contents
- 1 × 750 g net spool of black Recreus Reciflex, 1.75 mm.